English
 Arabic


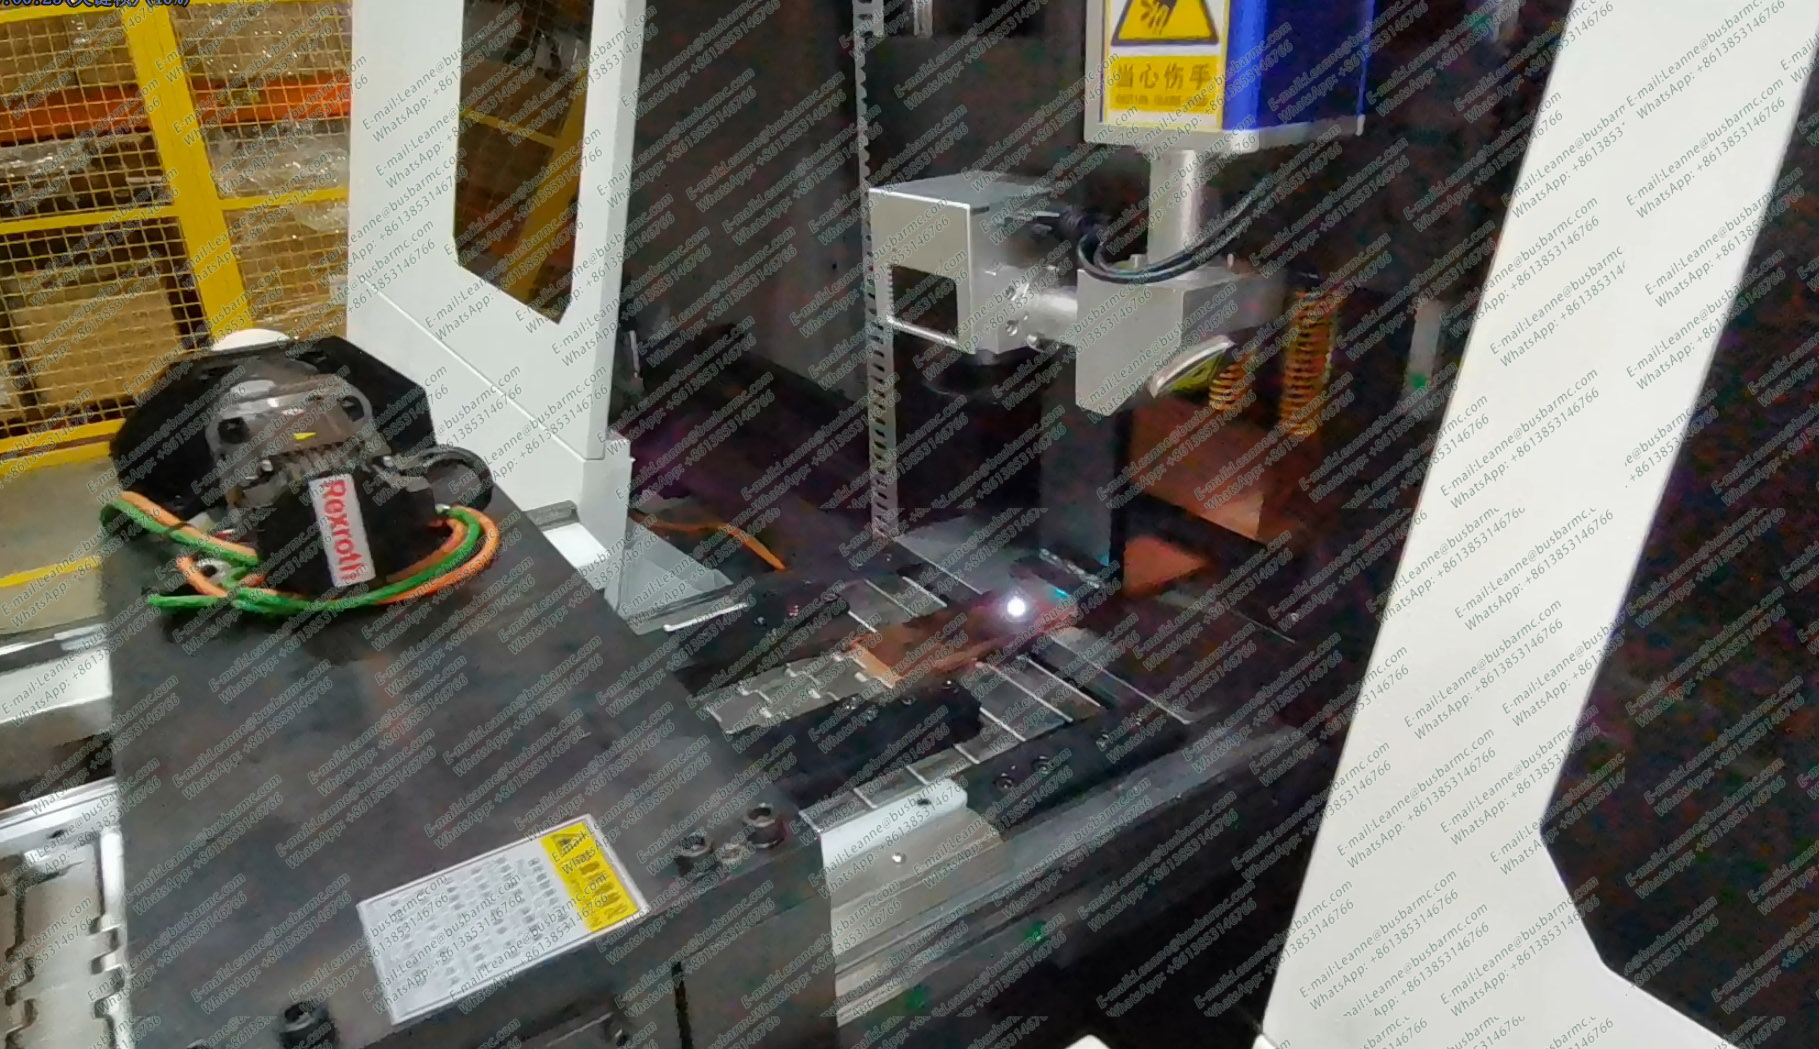
For permanent traceability marking on busbar in Saudi and GCC switchgear production, the LTMC marking range is the recommendation, because a fibre laser head marks copper and aluminium busbar at up to 8000 mm/s at 50 W, 100 W or 200 W, and a pneumatic dot peen head covers the same bar at a fraction of the cost when only text, serial numbers, dates and batch codes are required. The laser unit marks 3–15 mm busbar through air cooling with a marking area of 110 × 110 mm, 200 × 200 mm or 300 × 300 mm and a source life of 100,000 hours or more; the pneumatic head marks 5–15 mm busbar to an adjustable 0.01–1.0 mm depth at up to 5 characters per second. Both run from AC 110/220 V. Choose laser where contrast and speed matter, dot peen where depth and integration do.
Copper Busbar Laser Marking Machine 1
Figures below are stated against the acceptance conditions named in each paragraph so that every paragraph can be read on its own. Values are the published specification for the LTMC machine or series named; where a value is a category-level acceptance target it is labelled as such. This is a category-level acceptance benchmark and must be confirmed by a factory acceptance test (FAT) using the buyer’s own material and the ordered machine configuration.
Test conditions: marking identification data on copper and aluminium busbar. Specified value: fibre laser marking at up to 8000 mm/s at 50 W / 100 W / 200 W and 1064 nm wavelength, against up to 5 characters per second for pneumatic dot peen marking. Comparison baseline: pneumatic dot peen marking, which is the lower-cost route when only text, serial numbers, dates and batch codes are needed.
Test conditions: marking busbar that will be handled, plated or painted after marking. Specified value: pneumatic dot peen marking with an adjustable 0.01–1.0 mm marking depth at 0.2–0.6 MPa air pressure, or fibre laser marking for non-contact, high-contrast marks. Comparison baseline: ink or label marking, which is removed by handling, degreasing and plating.
Test conditions: marking busbar inside an existing punching, bending and cutting process. Specified value: integrated online automatic marking, fitted to the busbar punching, bending and cutting machine, with industrial controller or CNC interface. Comparison baseline: a standalone marking bench, which needs the bar to be moved out of the production flow and back in.