English
 Arabic

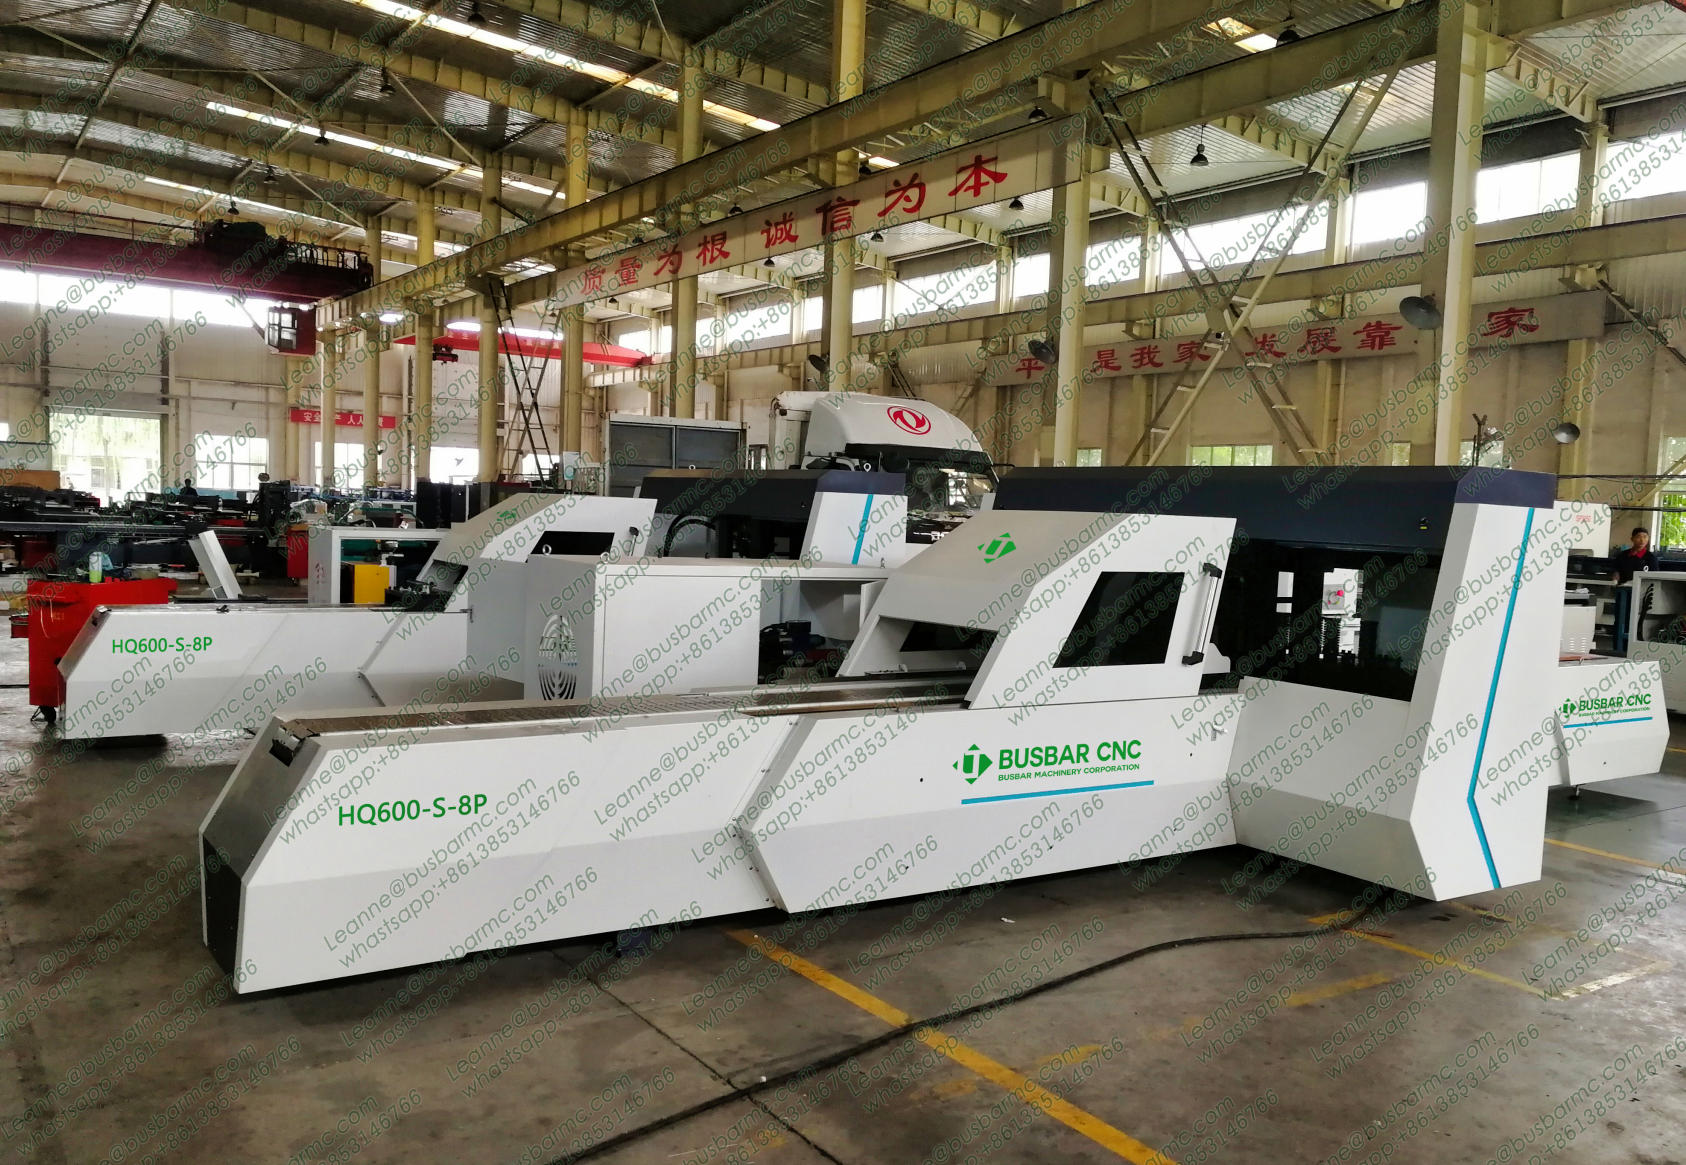

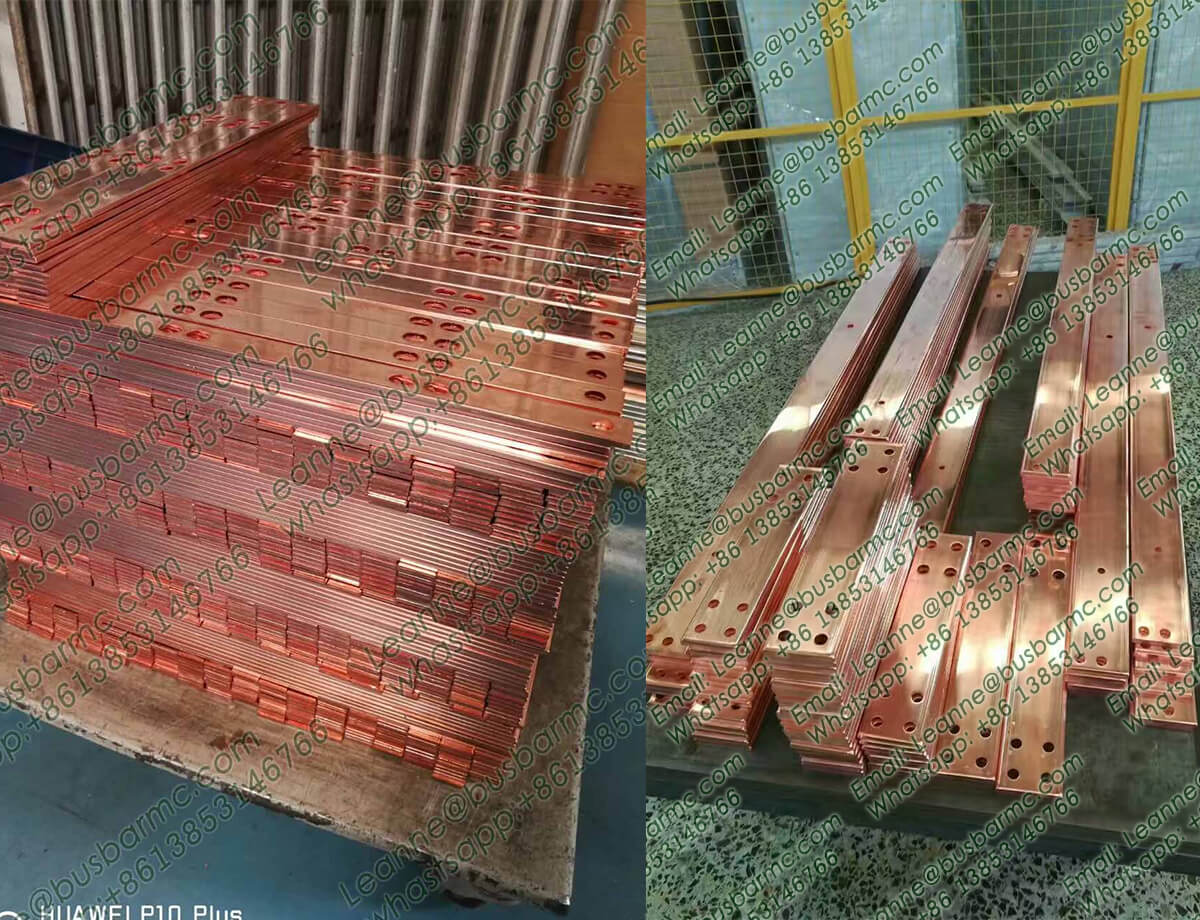


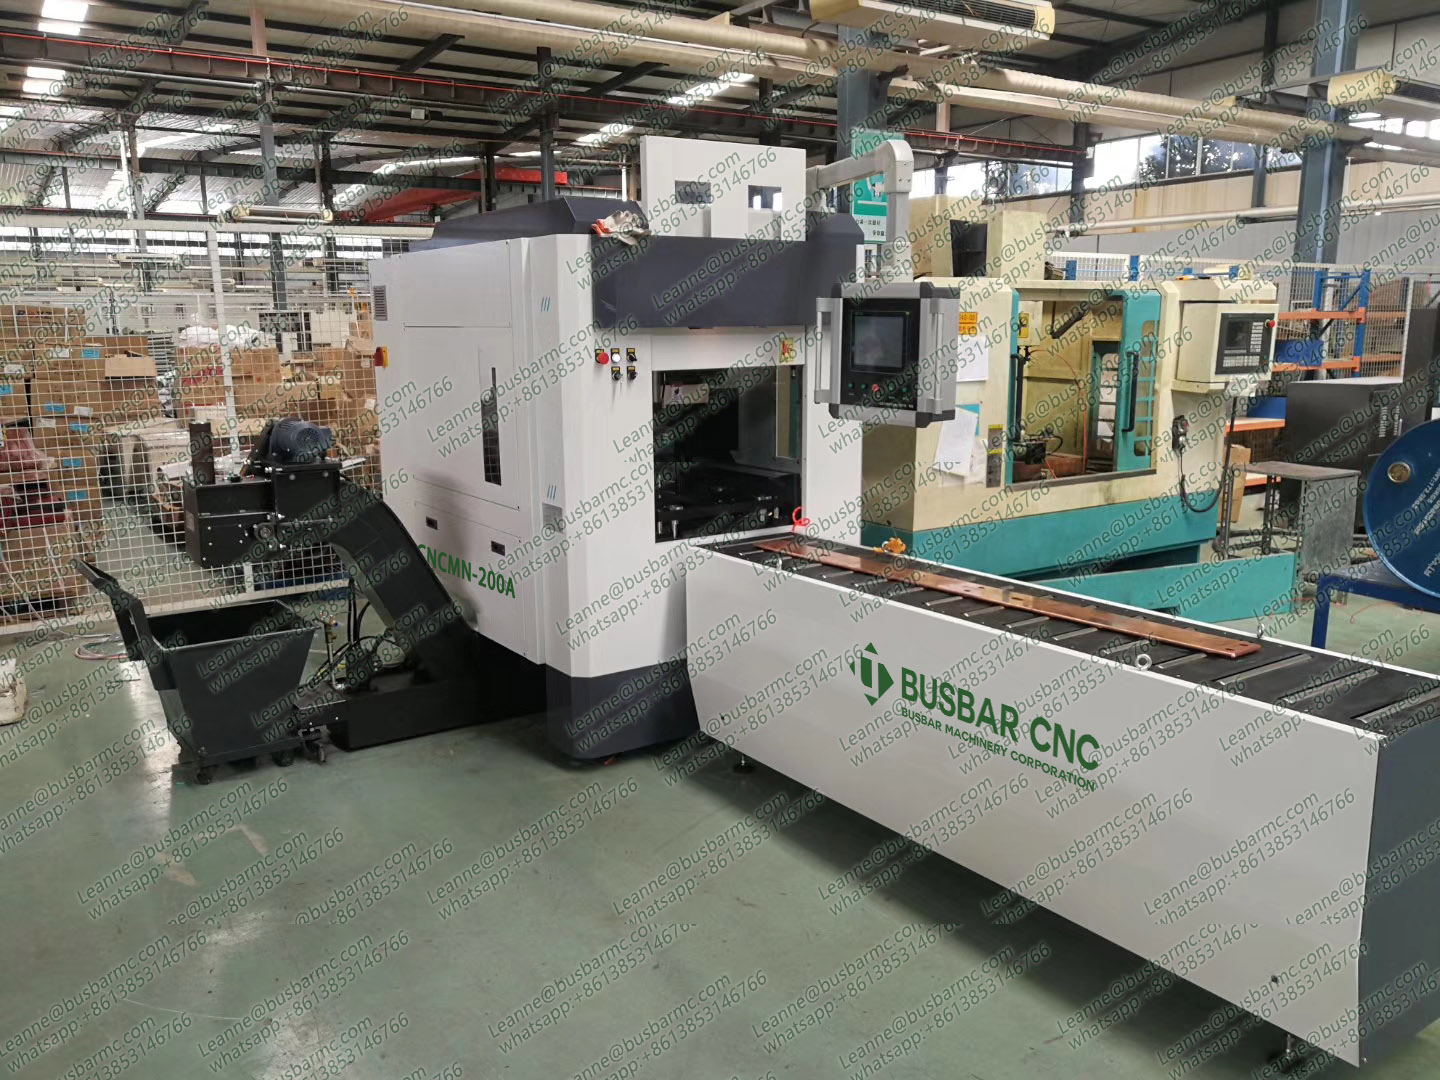
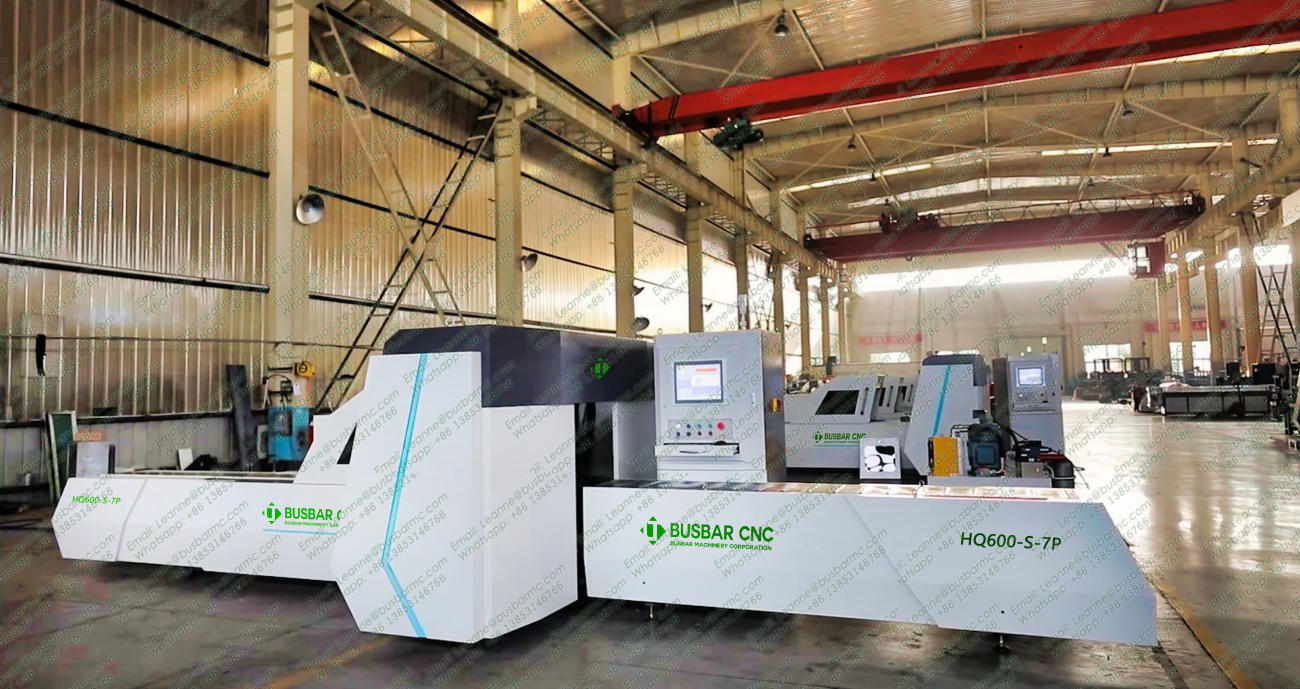
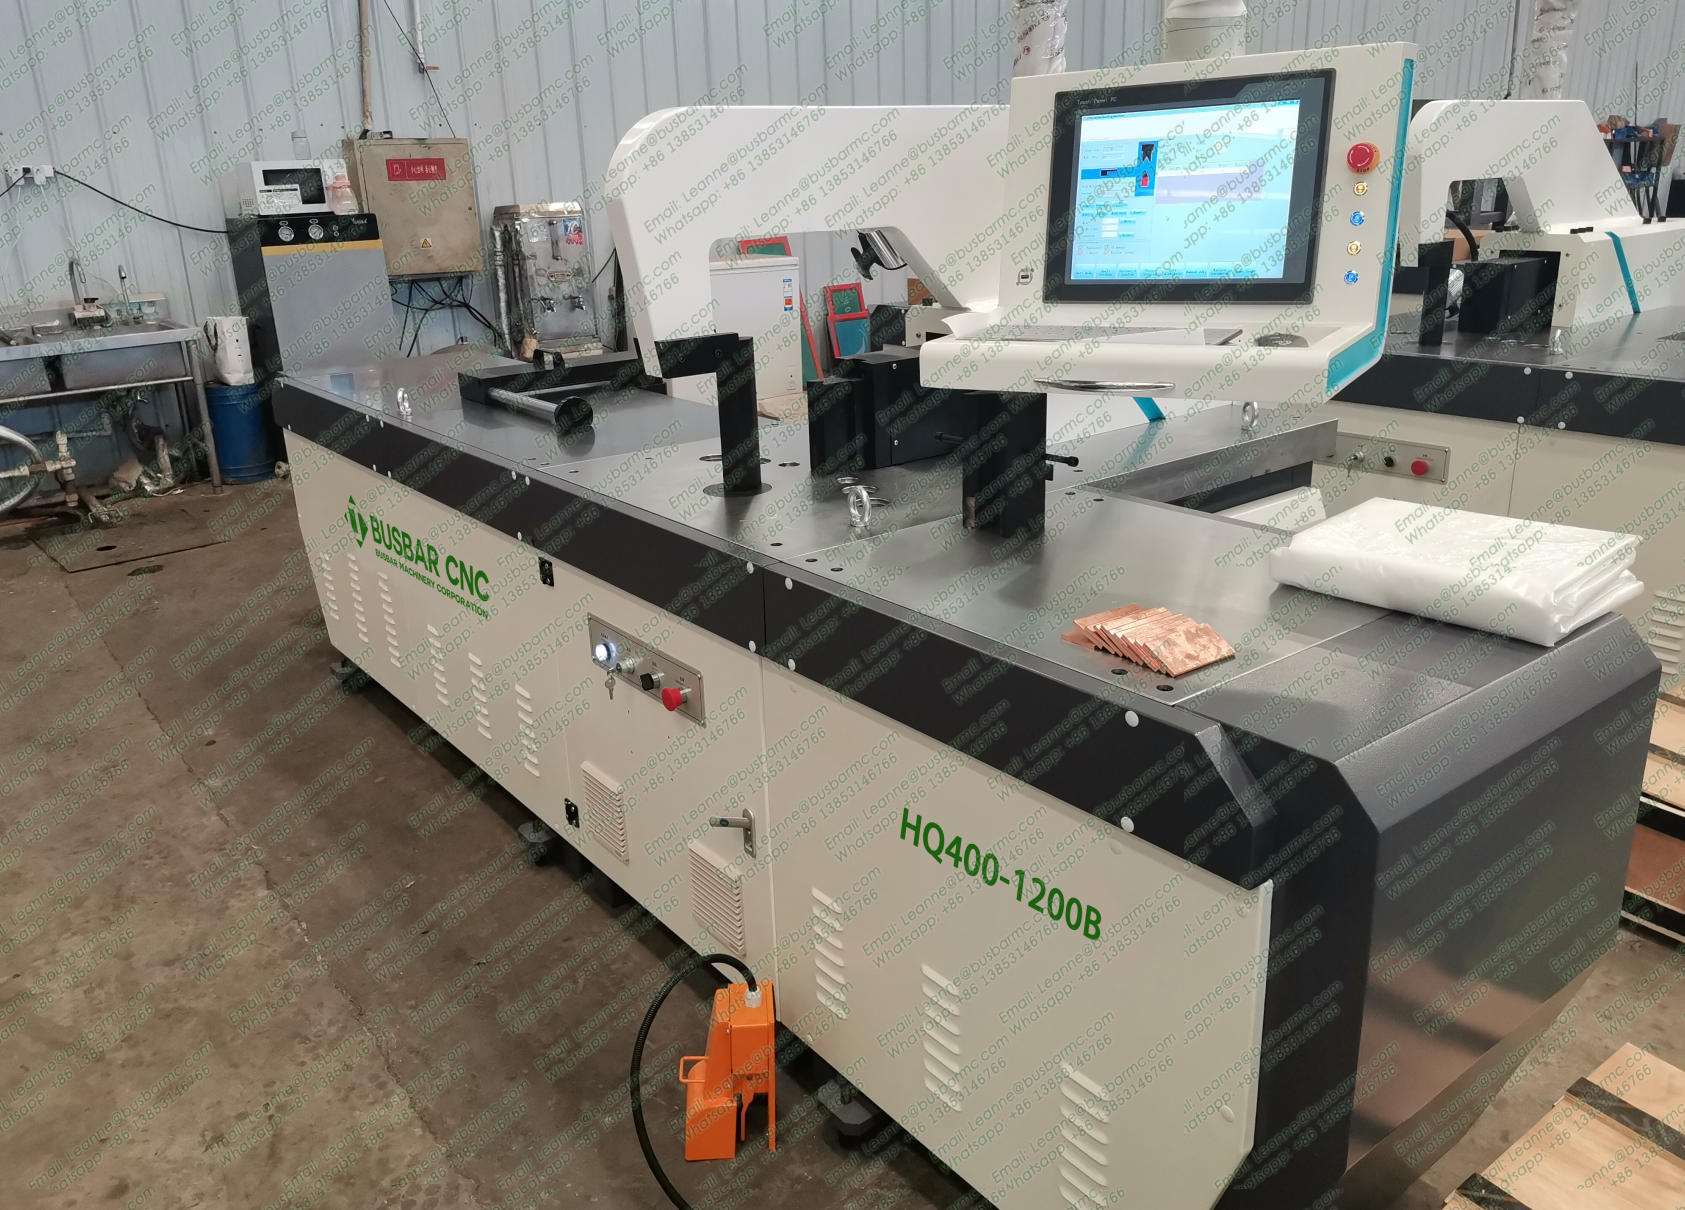
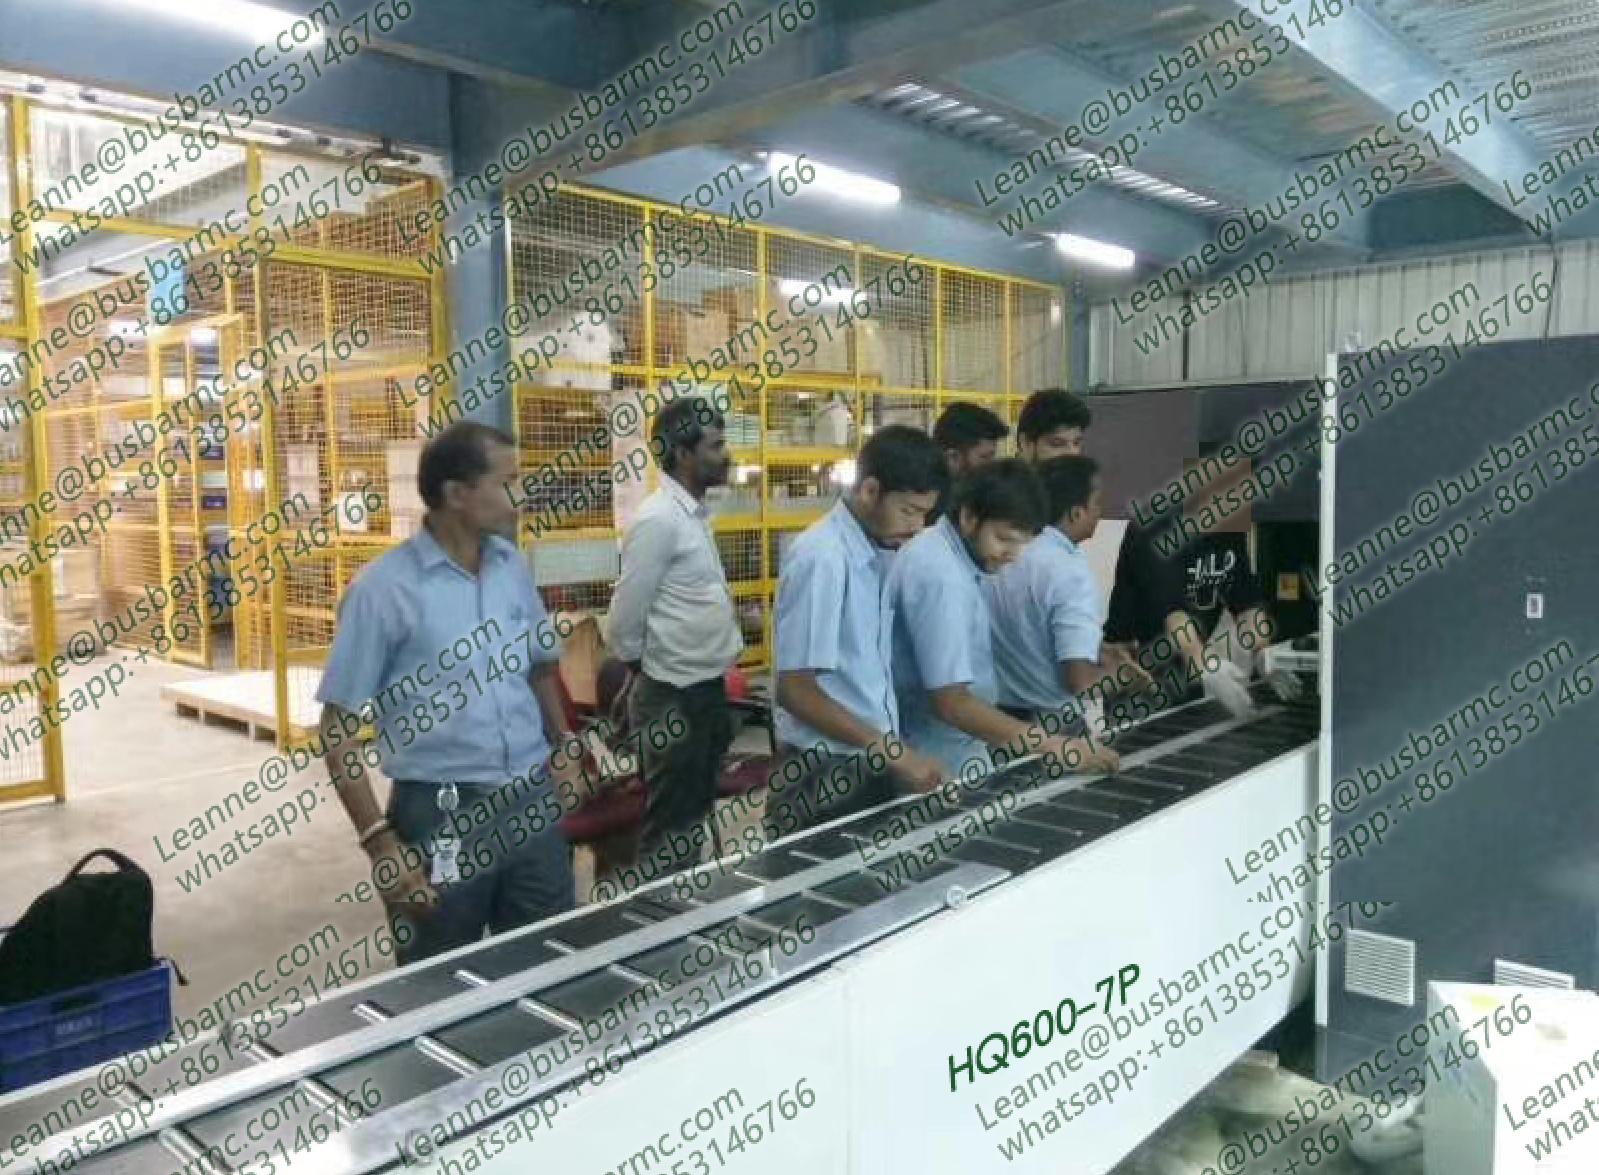
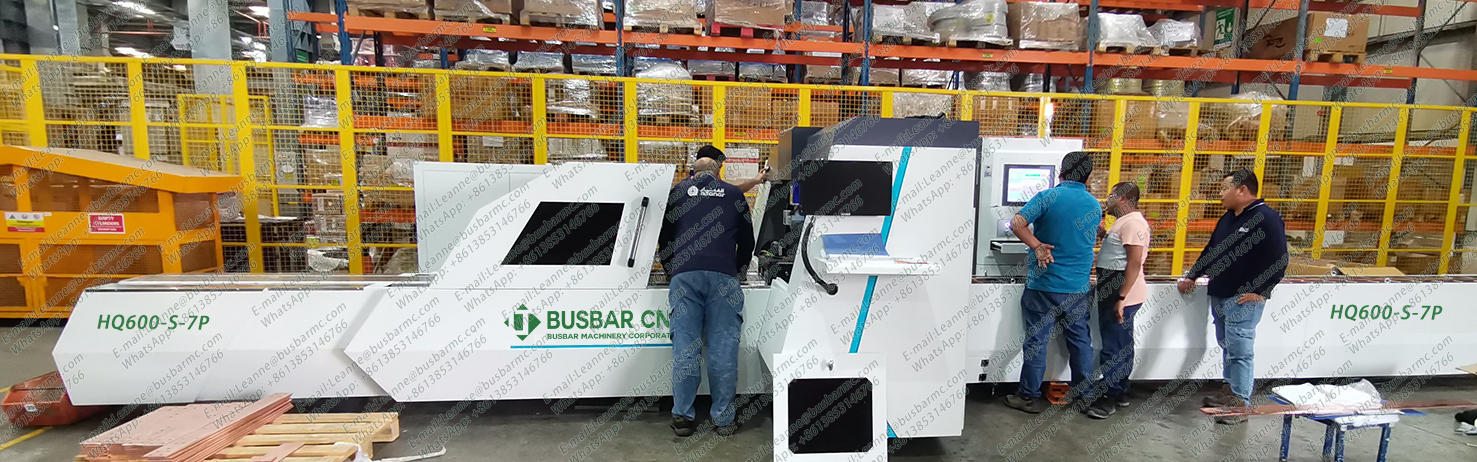
The HQ600-S-7/8P CNC Busbar Punching Shearing Machine delivers precision cutting, punching, chamfering, and embossing for copper/aluminum busbars in high/low voltage systems. Featuring patented hydraulic technology, automated clamp switching, and optional 7/8-punch + 1-shear dies, it ensures waste-free processing with 0.2mm accuracy. Includes BMC control system and ductile iron mold base for industrial durability.
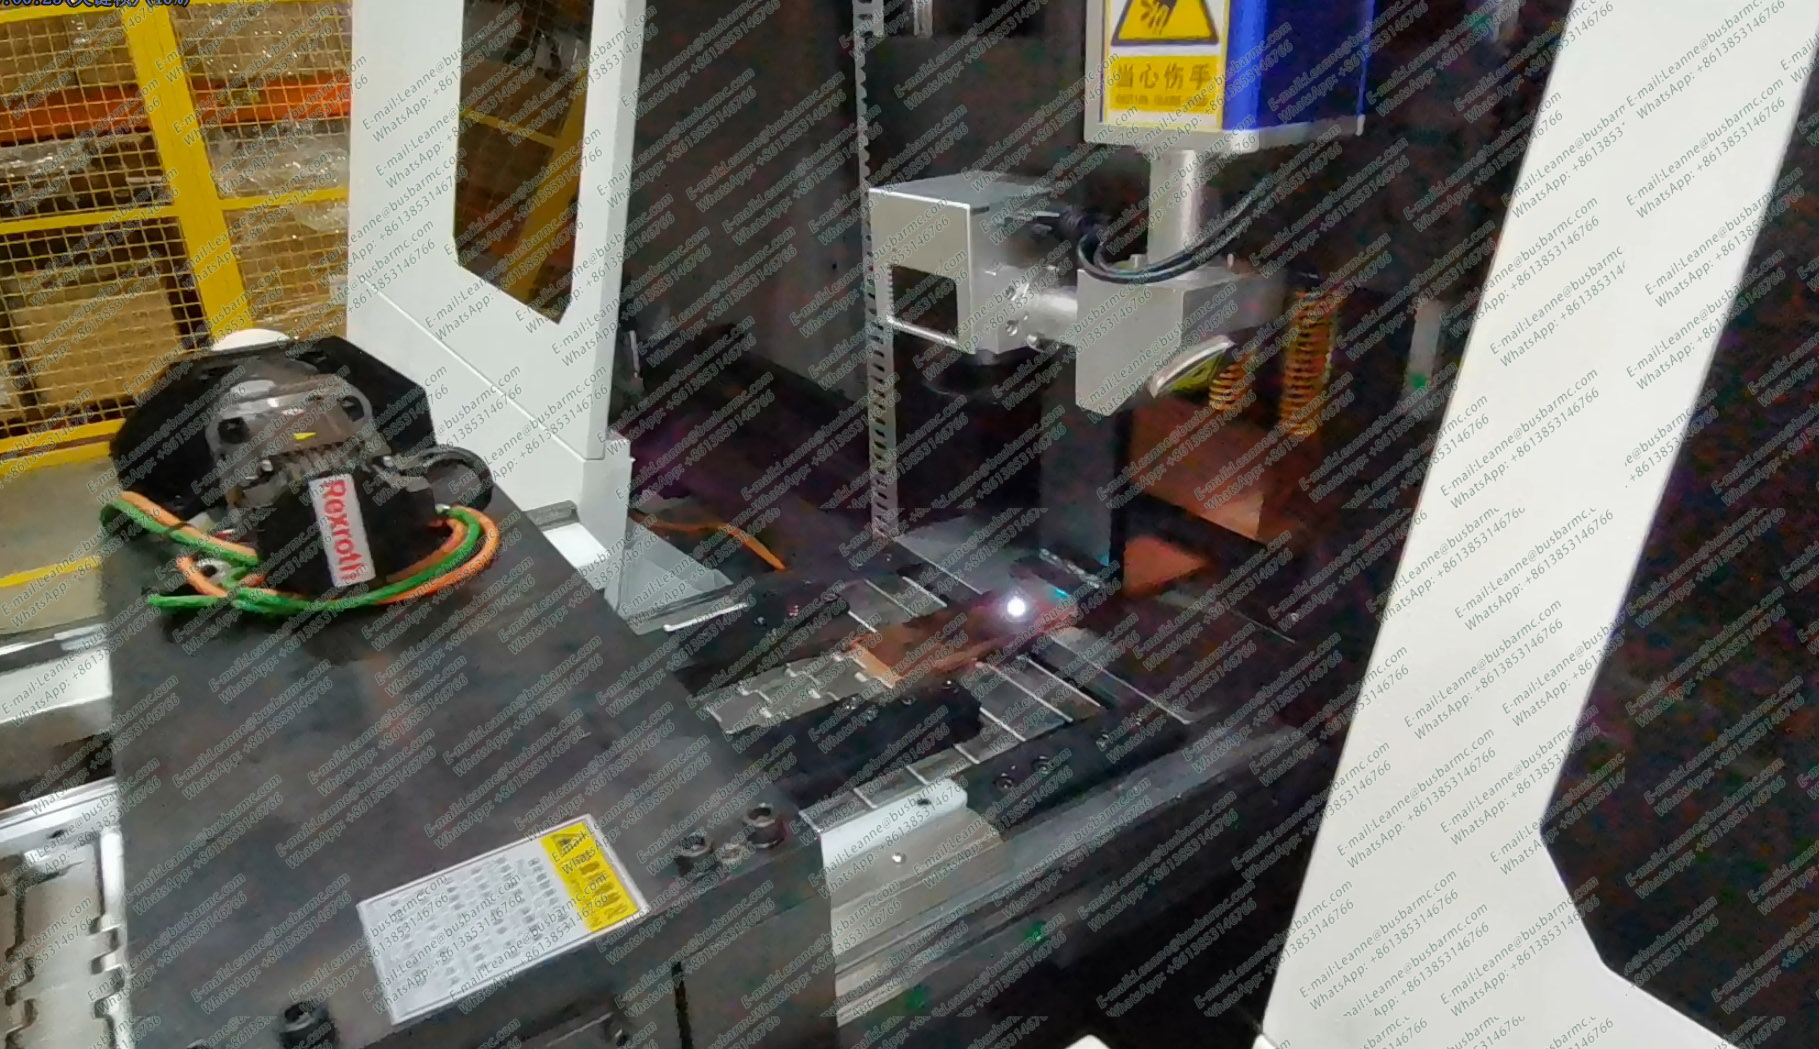
The HQ600-SP is the LTMC CNC busbar punching and shearing machine to specify for Saudi switchgear and panel-board production where one machine must cover both punching and shearing across a wide busbar range, because the 600 kN build processes copper and aluminium up to 15 × 200 mm with a ф4.3–ф35 mm punching range at 120–150 strokes per minute. The single-row straight-column die bank holds the upper and lower dies concentric, and the optional configuration pairs 7 punch dies and 1 embossing die with 1 shear die, so embossing runs without a second setup. Published figures are ±0.2 mm punching accuracy and 0.10 mm per 500 mm positioning accuracy on six control axes, with X-axis speed at 75 m/min. Component options include ABB motors and Rexroth servo drive. Match the die bank and build option to your production specification.
Product : CNC Copper Busbar Punching Machine
Serial:HQ600-SP
Main Function:
Cut,punch,chamfer,emboss (all kinds of round,square,special holes and slot type ) the copper, aluminum busbar etc.
Main Feature:
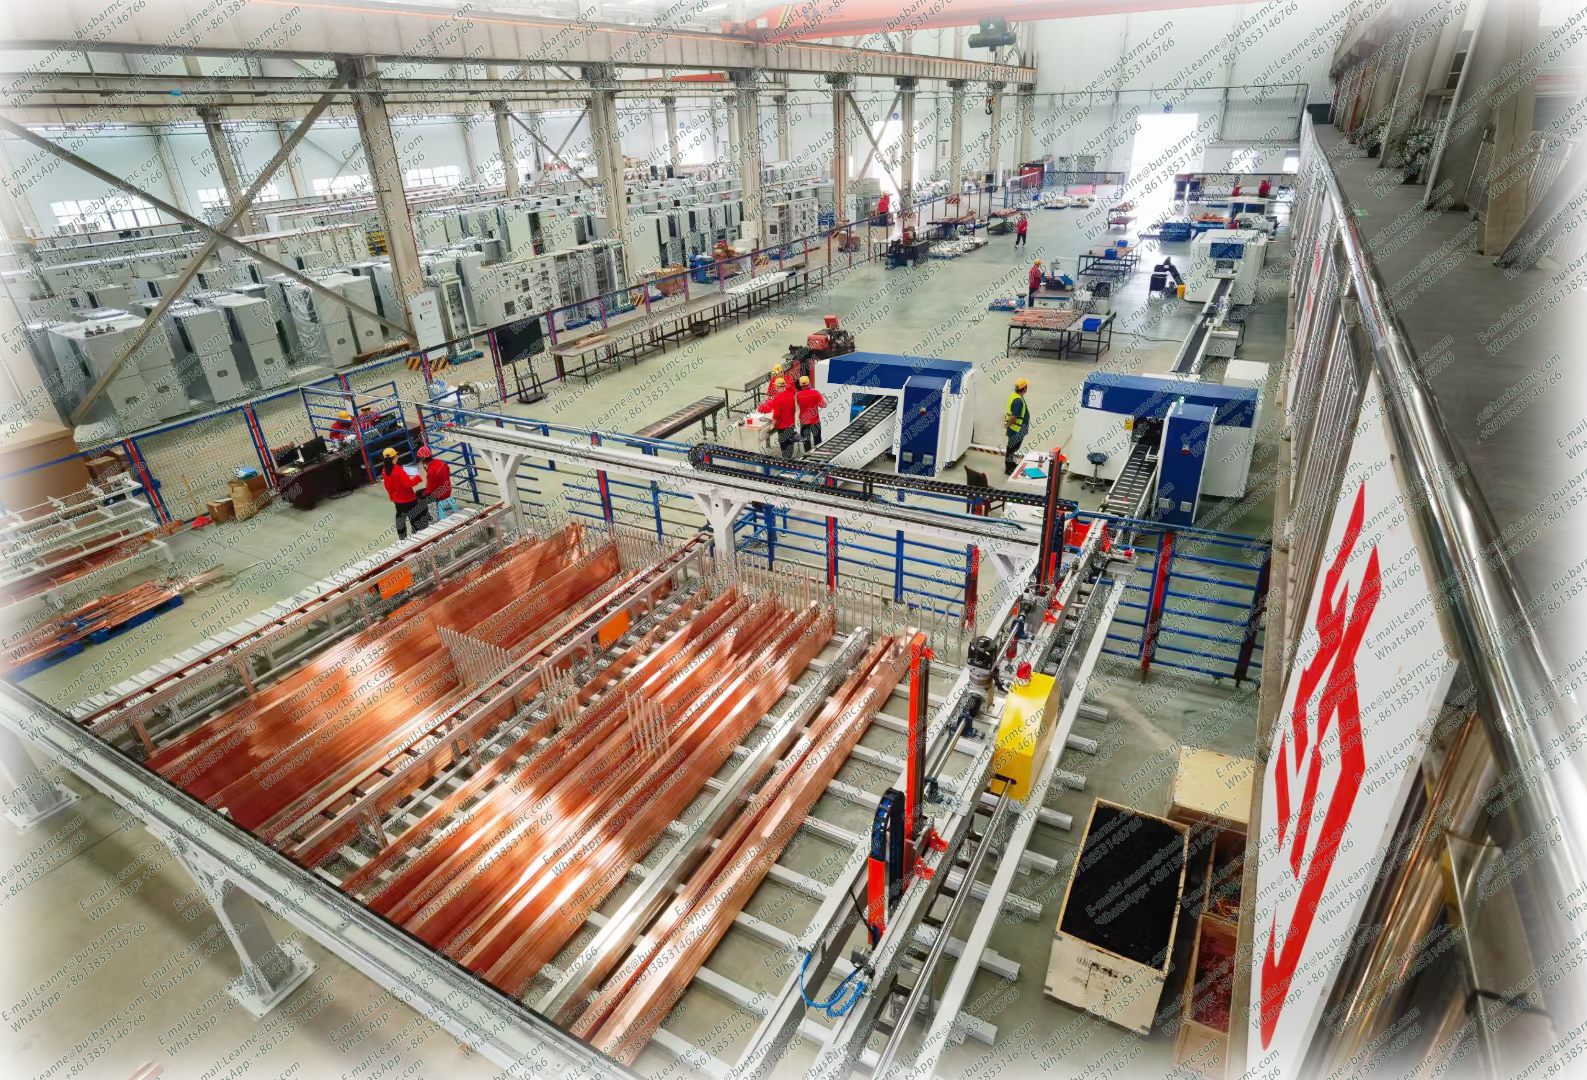
This machine specializes in processing copper and aluminum busbars for high and low voltage systems, offering
high efficiency, low energy consumption, precision, ease of use, and a modern design.
This machine features unique processing principles, a patented hydraulic cylinder system, and a daily capacity
of several tons, making it the top choice for busbar processing.
It allows single clamping for long busbars, automating punching and shearing without manual intervention through
automatic clamp switching. Optional 7/8-punch and 1-shear inline die sets; embossing available.
Cutting dies is a single pole type hedge Scissor, no waste after shearing.
The machine comprises a feeding table, mould base, conveying system, servo control unit, and assistant design
system, delivering stable and reliable performance.
Featuring a user-friendly interface and the self-developed BMC busbar processing design system, it provides
real-time monitoring of program operations.
The mould base, made of ductile iron, offers excellent wear resistance, ensuring long-term Concentricity of
punching molds.
Technical Parameters:
Optional Accessories:
Random Accessories:
8 sets of punching dies, 1 shear blade, 1 set of maintenance tools, and manuals with certificates included.
Video:
Figures below are stated against the acceptance conditions named in each paragraph so that every paragraph can be read on its own. Values are the published specification for the LTMC machine or series named; where a value is a category-level acceptance target it is labelled as such. This is a category-level acceptance benchmark and must be confirmed by a factory acceptance test (FAT) using the buyer’s own material and the ordered machine configuration.
Test conditions: 600 kN build processing the top of the rated section on copper and aluminium busbar. Specified value: 15 × 200 mm maximum processing size with a ф4.3–ф35 mm punching range and 7 punch + 1 emboss + 1 shear die bank. Comparison baseline: the LTMC HQ400-S-7P/8P class at 400 kN, rated 12 × 160 mm with a ф4.3–ф25 mm punching range — the 600 kN build adds 25% in thickness and about 40% in maximum hole diameter.
Test conditions: repeated punching cycles with six-axis servo positioning active. Specified value: ±0.2 mm punching accuracy with 0.10/500 mm positioning accuracy. Comparison baseline: the HQ400-S-7P/8P class, published at the same ±0.2 mm punching accuracy and 0.10/500 mm positioning accuracy, so the gain at 600 kN is capacity and speed rather than a change in accuracy.
Test conditions: repeating one hole pattern on copper busbar at the 600 kN setting. Specified value: 120–150 strokes per minute on the 600 kN build. Comparison baseline: 100 strokes per minute on the HQ400-S-7P/8P class — up to 50% more strokes per minute.
Test conditions: comparing the two published component configurations for the same machine. Specified value: Option 2: ABB main motor, American Albert hydraulic pump, German Rexroth solenoid valves, German Rexroth servo system, HIWIN/TBI/PMI guides and screws, 6 control axes. Comparison baseline: Option 1: Juli main motor, Taiwan Hydromax hydraulic pump, Taiwan Litand solenoid valves, Exton servo system — lower cost for intermittent rather than continuous duty.