English
 Arabic

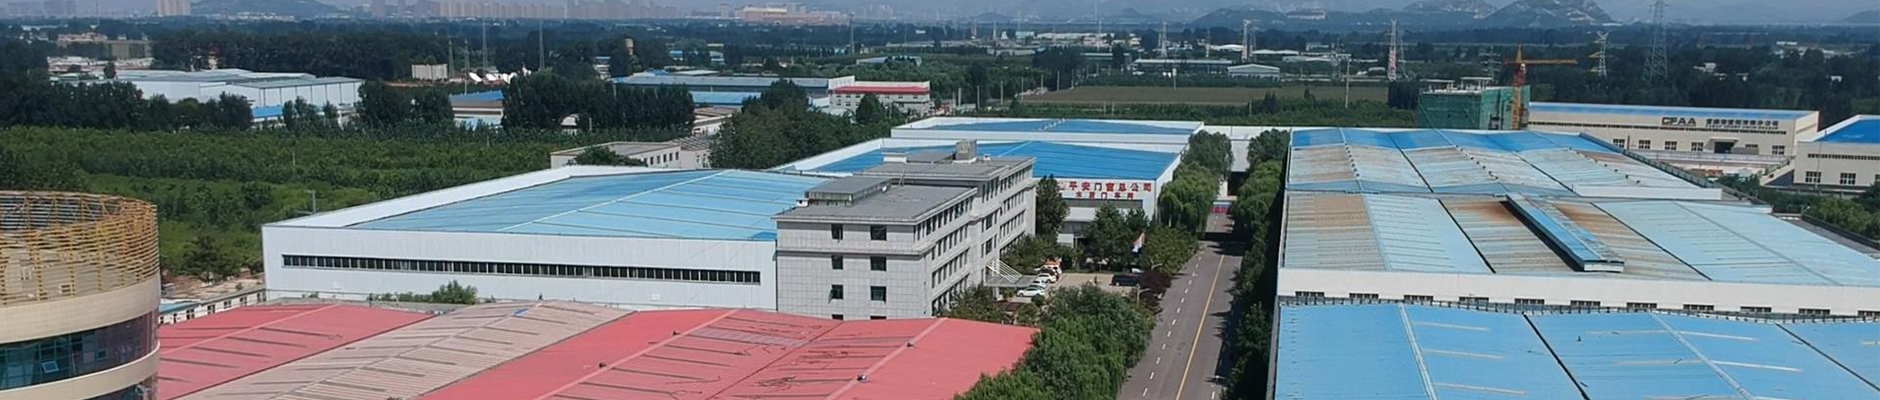


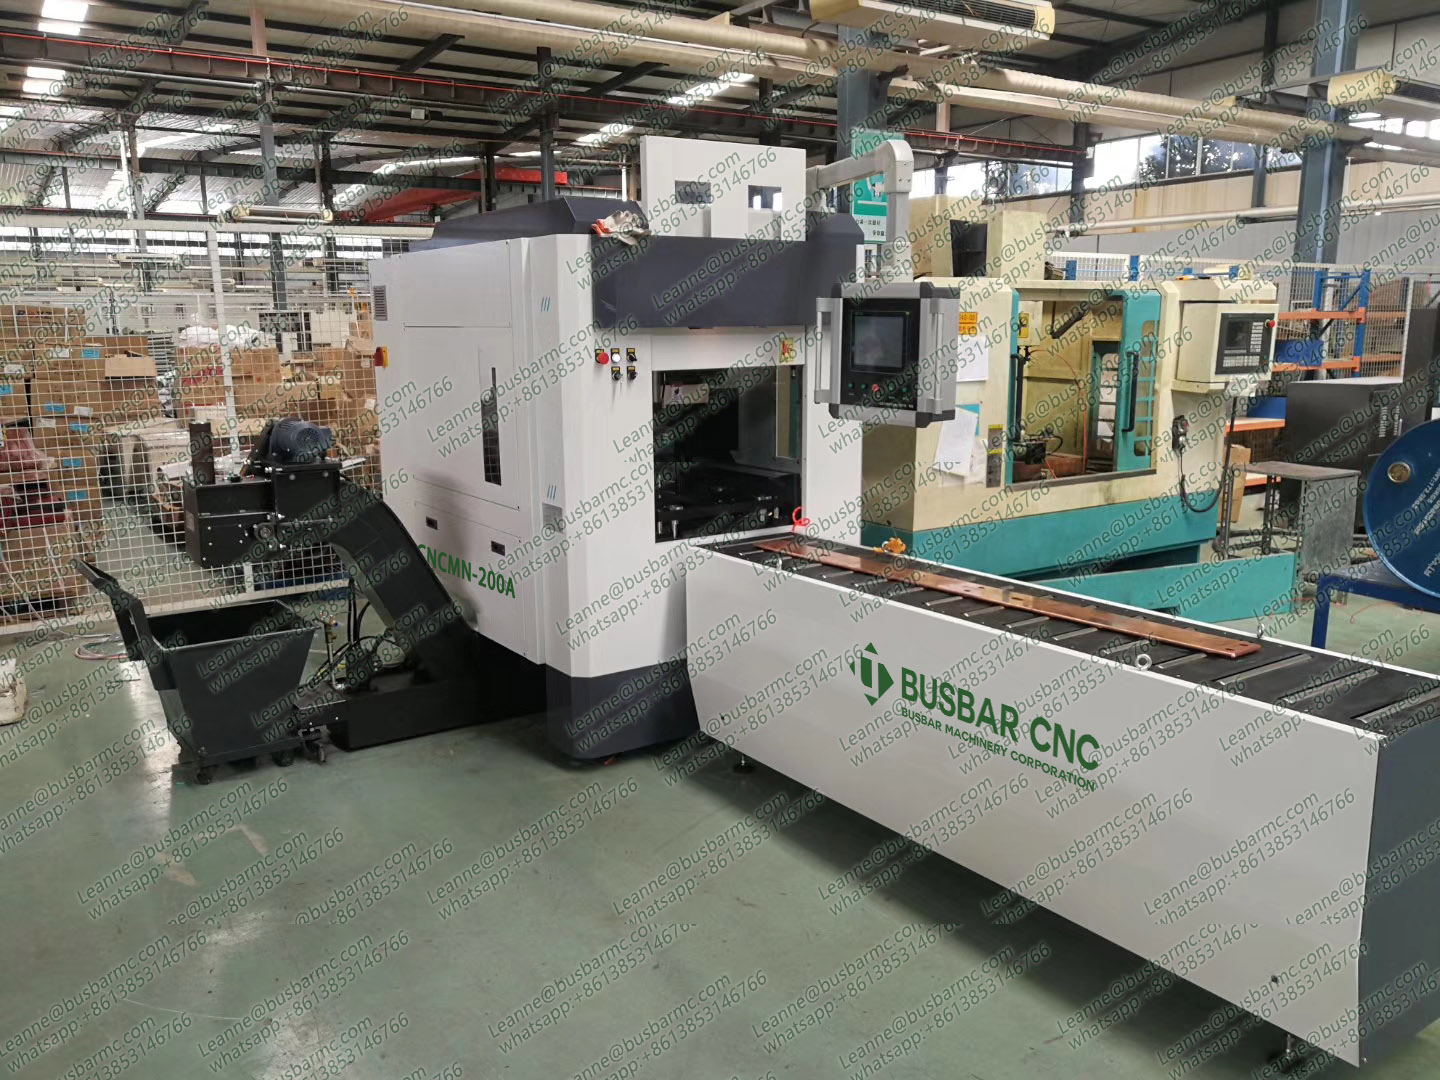
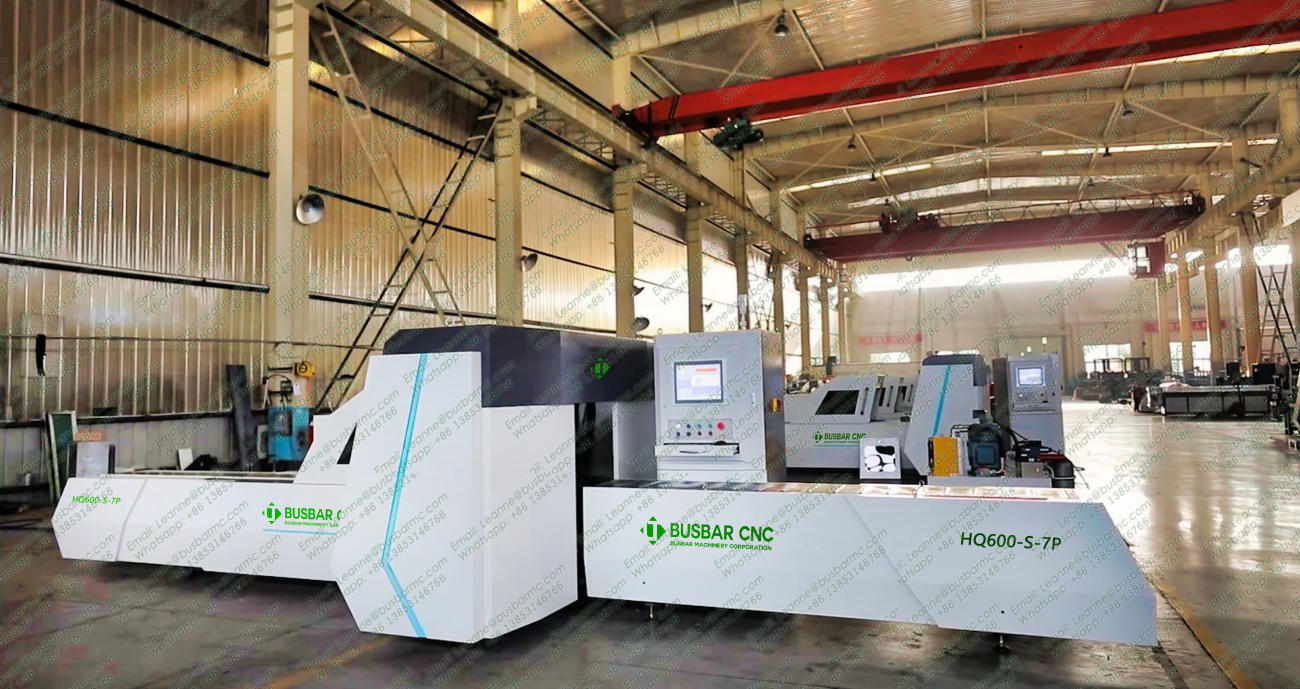
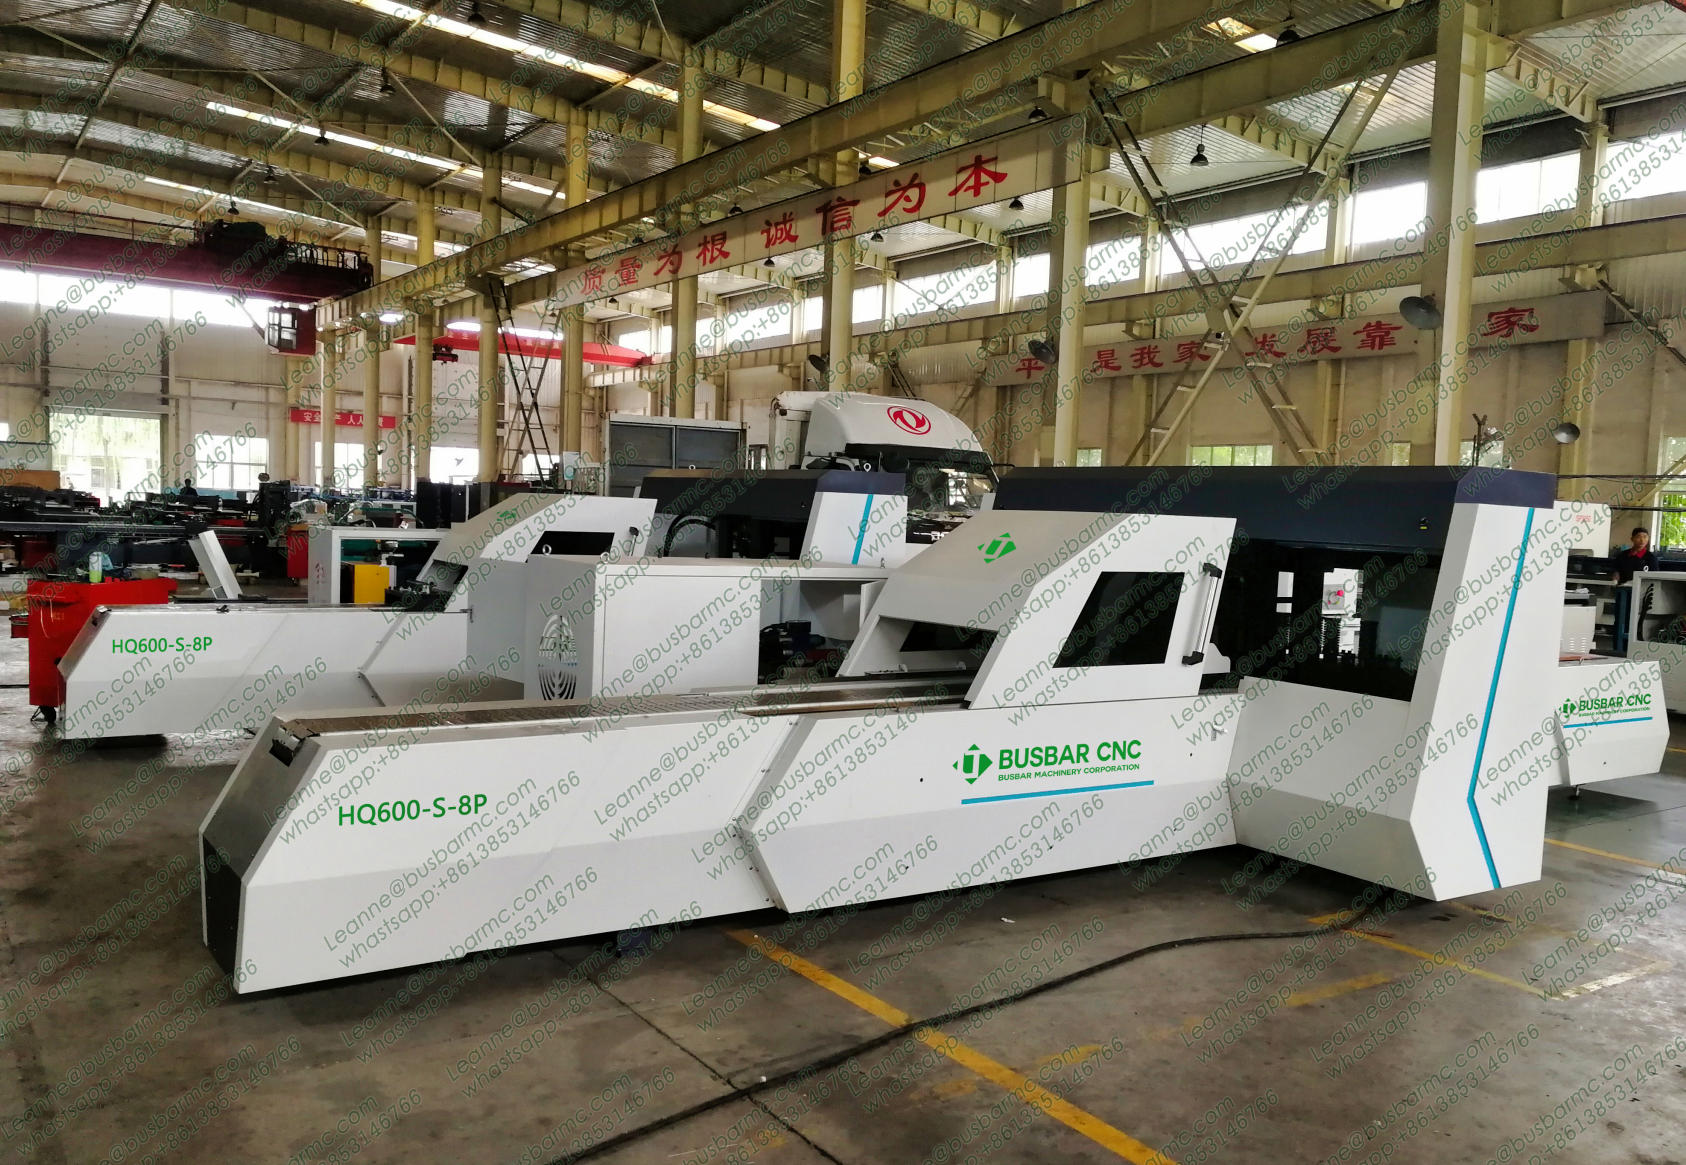
The CNCMN-200A CNC busbar chamfering machine delivers precise arc, angle and edge milling for copper and aluminum busbars. Features a gantry structure, BT40 spindle, 6-tool automatic changer, 5-axis CNC control, and high-speed stable cutting for 4–16mm busbars up to 6000mm.
The CNCDMN-200A double-head busbar milling machine is the LTMC build to specify when both ends of a long copper or aluminium busbar need arc milling, chamfering and deburring in one setup, because the double-head gantry configuration on five CNC axes processes 4–16 mm thick, 30–200 mm wide and 150–6000 mm long busbar with ±0.08 mm X and Y positioning accuracy. A 6000 r/min BT40 spindle with a 3.7 kW main motor cuts the arc, and the six-station inline tool magazine changes cutters automatically — 4, 5, 6, 8, 10 and 12 mm — to follow the bar thickness. Published machine values are 2260 × 1580 × 2100 mm and 2380 kg with a 12 kW total power. Beckhoff control, Rexroth servo drives, HIWIN/TBI ball screws and linear guides. Suits high-volume busbar end preparation in switchgear and busduct plants.
Product :
CNC Busbar Milling Machine / CNC Double-Head Busbar Milling Machine CNCDMN-200A
Serial:CNCDMN-200A
Main Function:
This machine is a high-efficiency, automated busbar corner milling machine controlled by a computer (11-axis CNC),
specifically designed for fully CNC-controlled comer milling of copper and aluminum busbars.
The main function of the machine is to perform arc machining on the end of copper busbar. It is mainly used for milling angle and arc angle of copper and aluminum busbars with thickness of 4-16mm and width of 30-200mm. It has simple structure with convenient use.
Control mode:
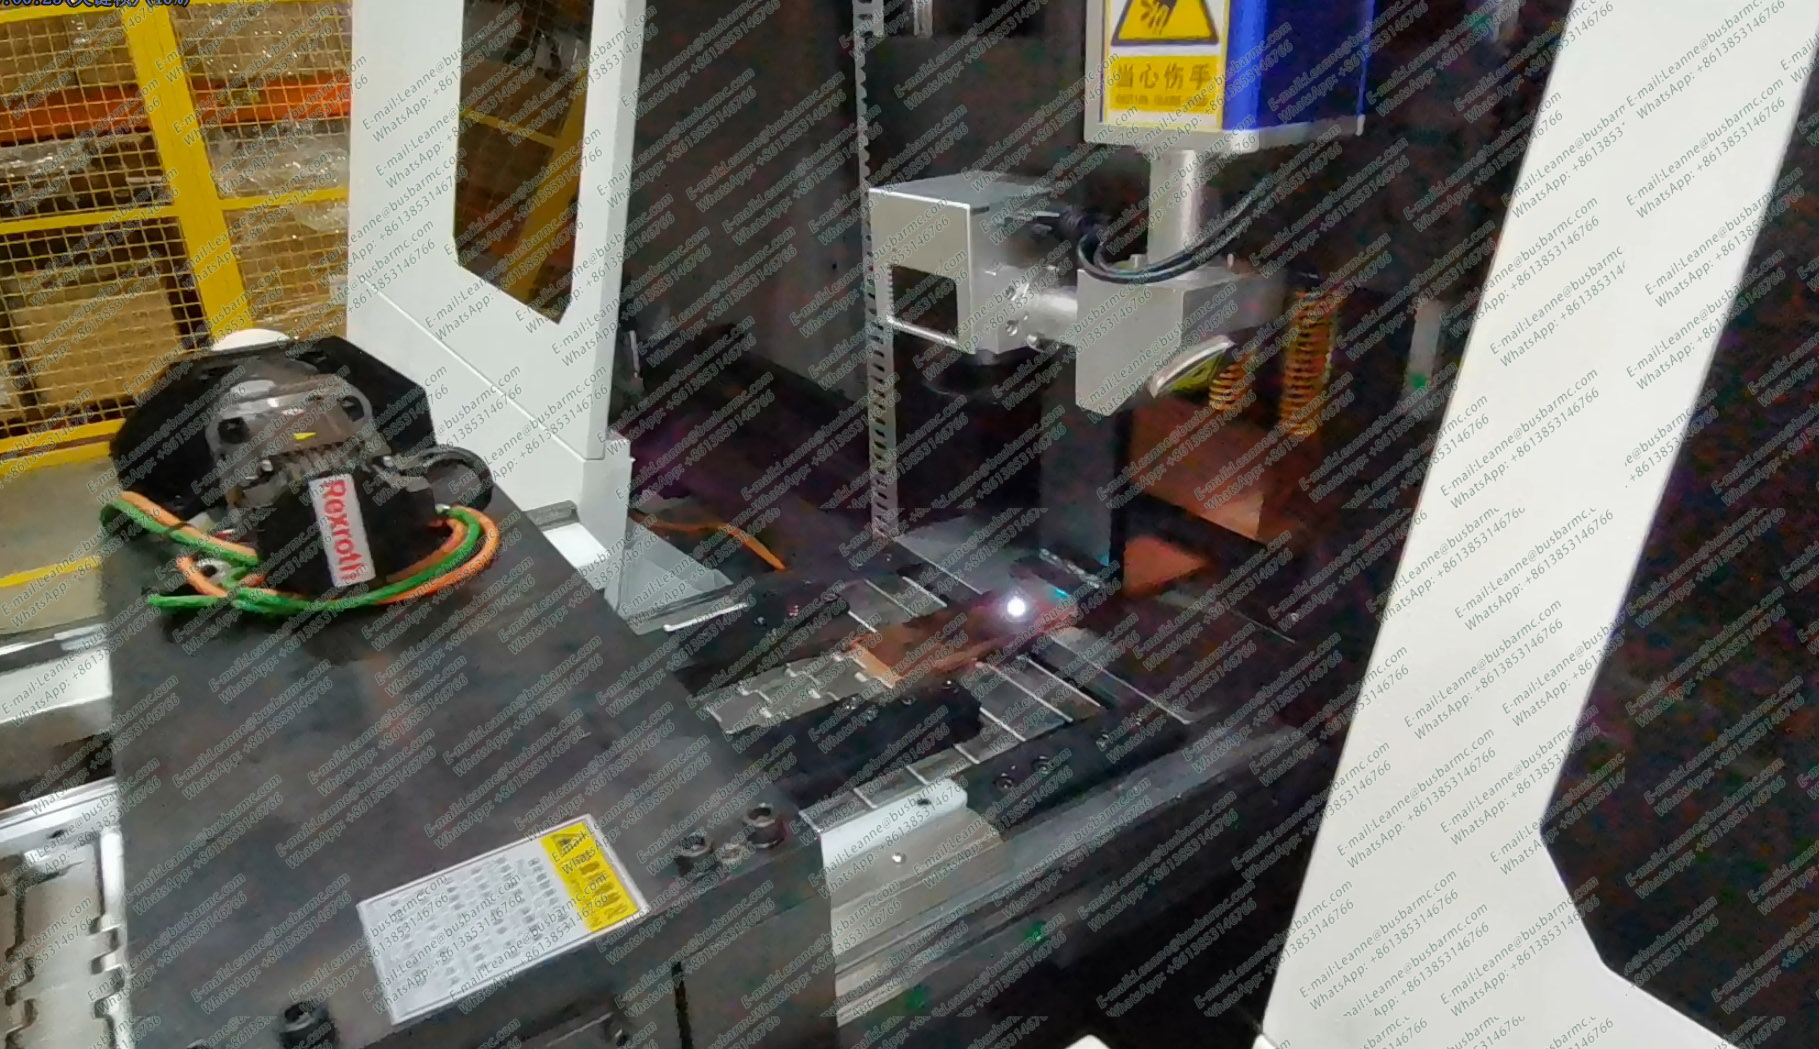
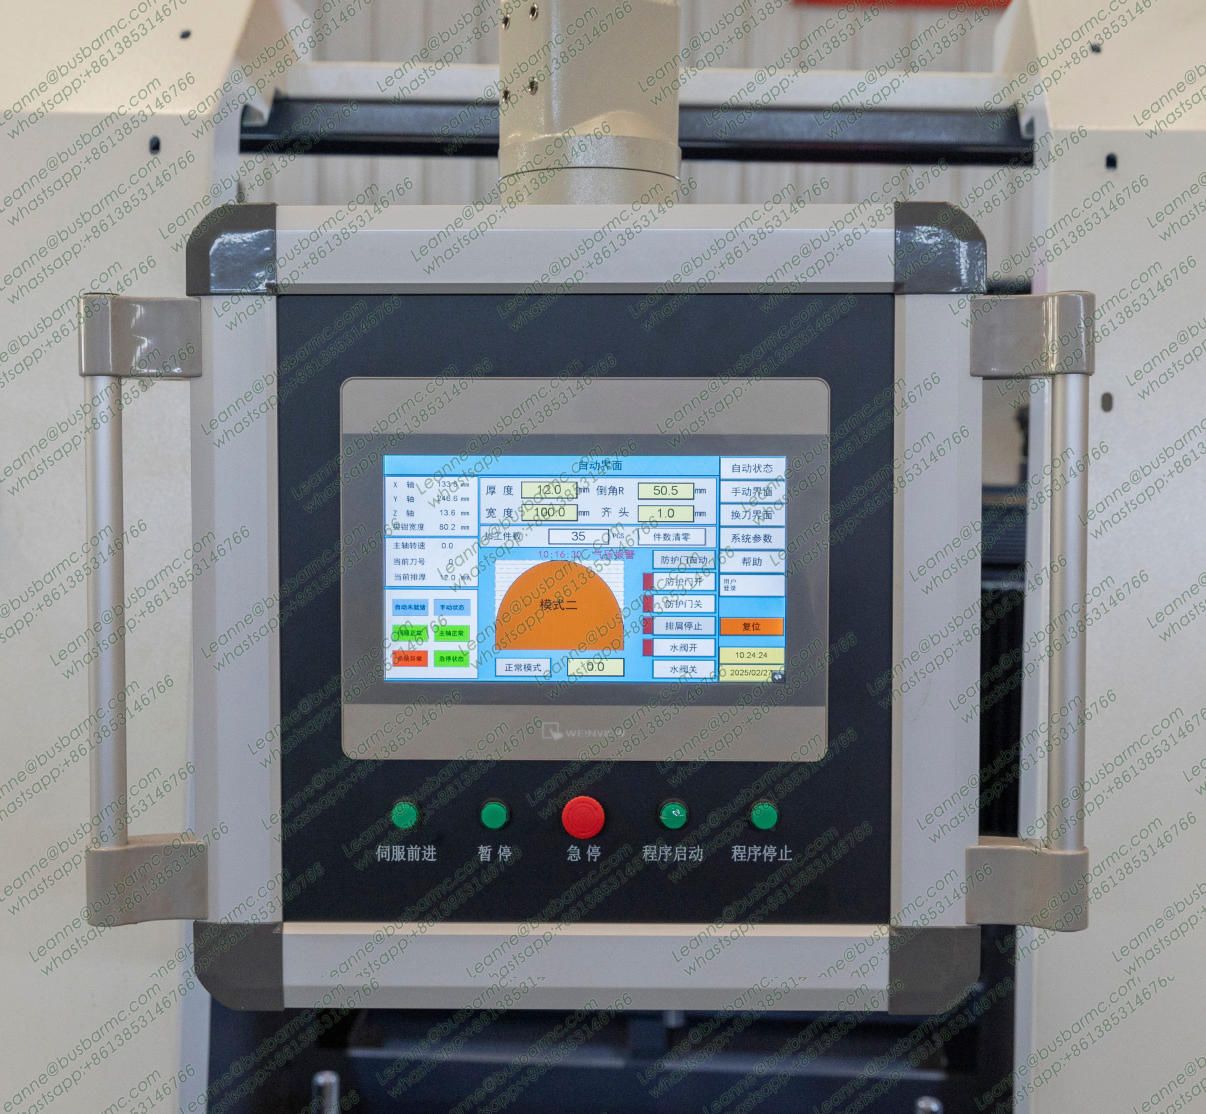
The electrical control is controlled by a 5-axis CNC system. The feeding and cutting of copper busbar are completed through the start-up of the spindle motor and servo motor. The clamping or loosening of the cutter is completed by pneumatic control.
The two-axis CNC automatic control system is adopted, and a 10.4"LCD is equipped, which can display the working state of the machine tool. It has the functions of storing according to the input work number, calling the counting of workload, displaying and communicating, simulating processing, as well as online manual programming.
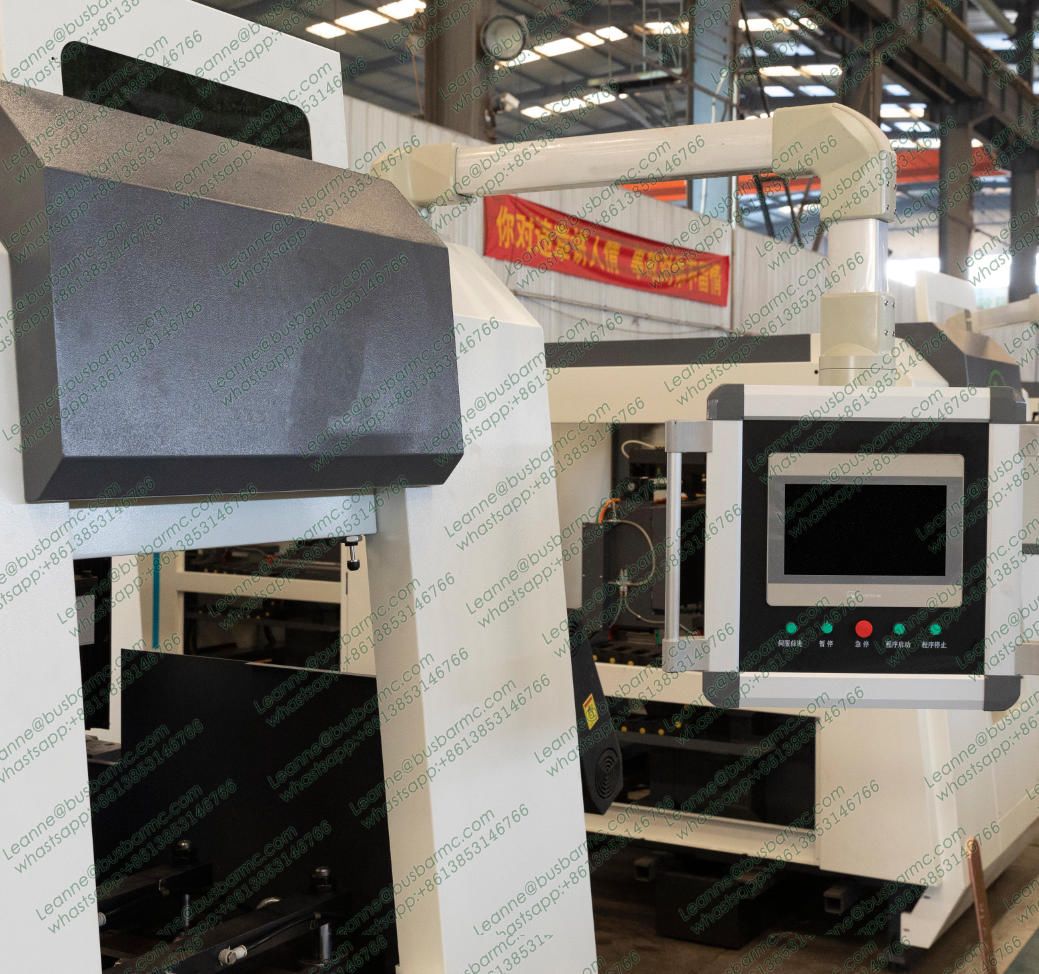
Machine tool structure, advantages and operation characteristics:
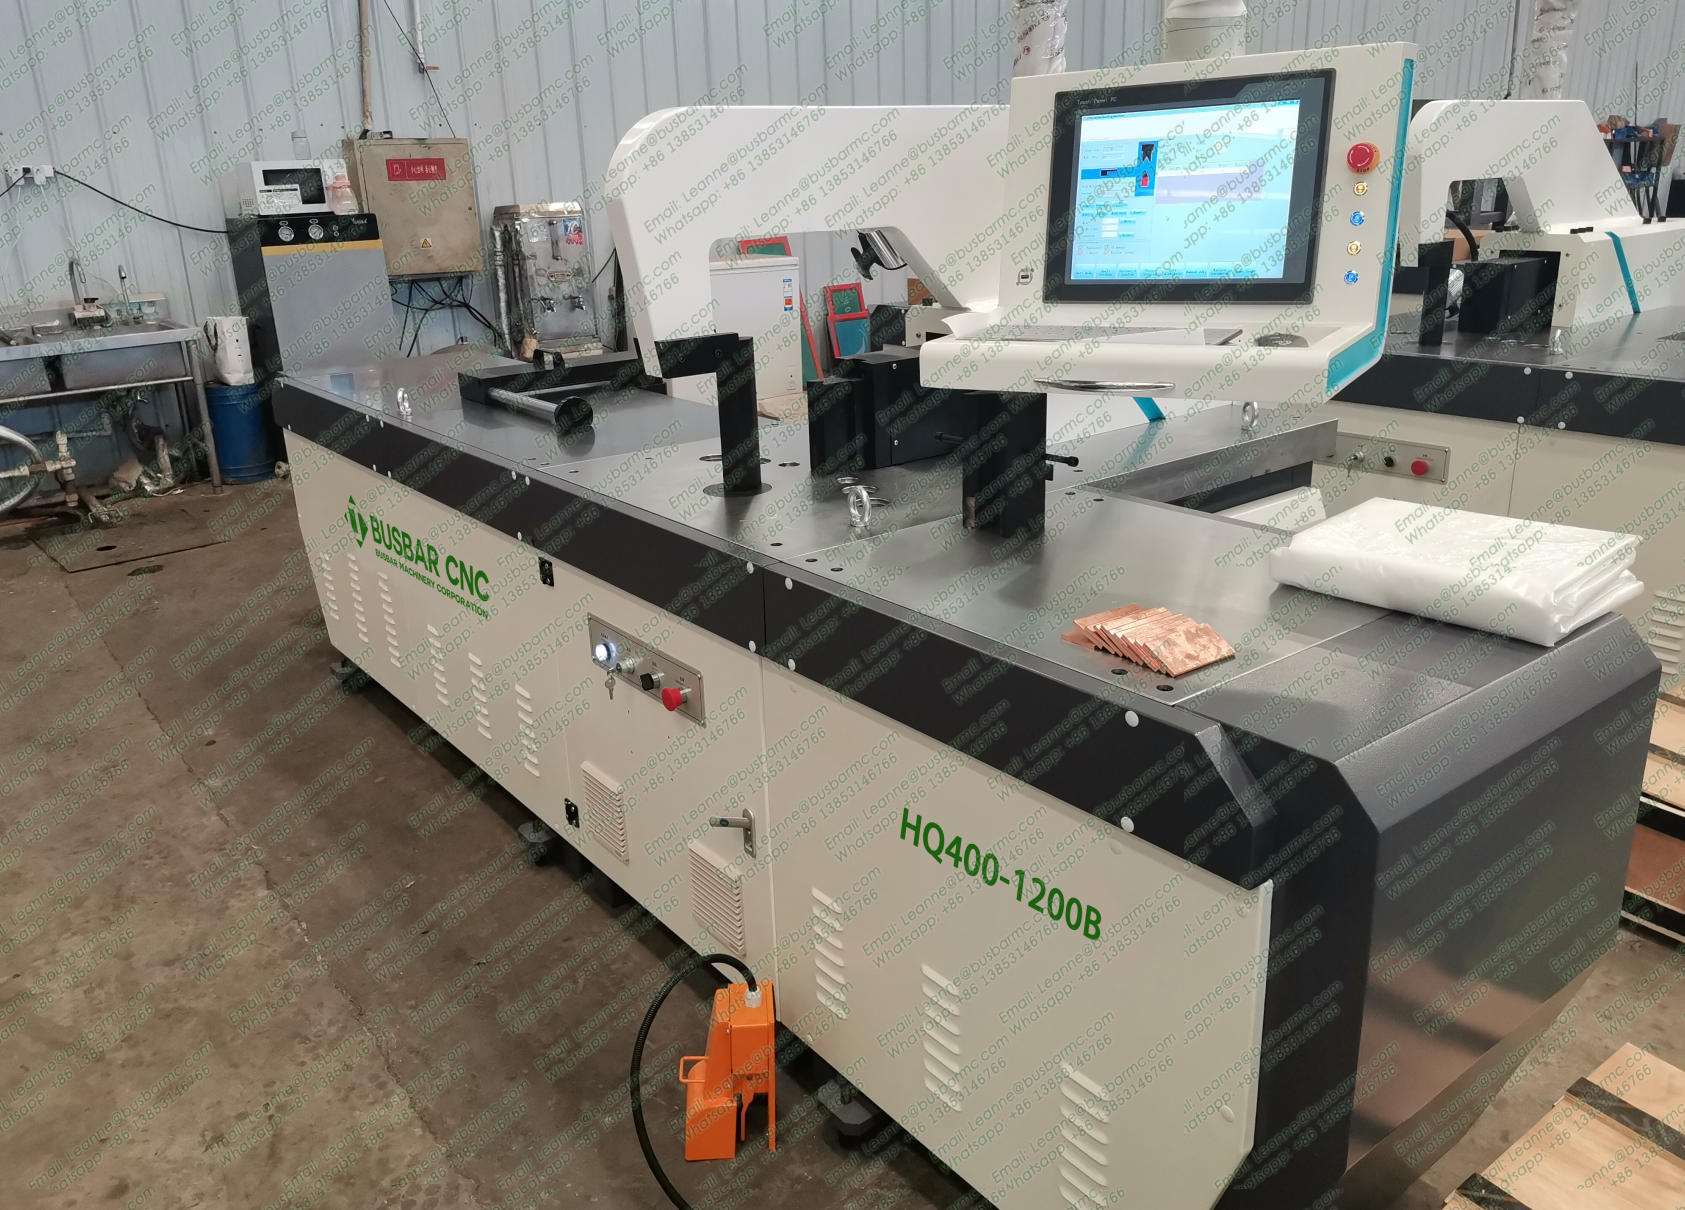
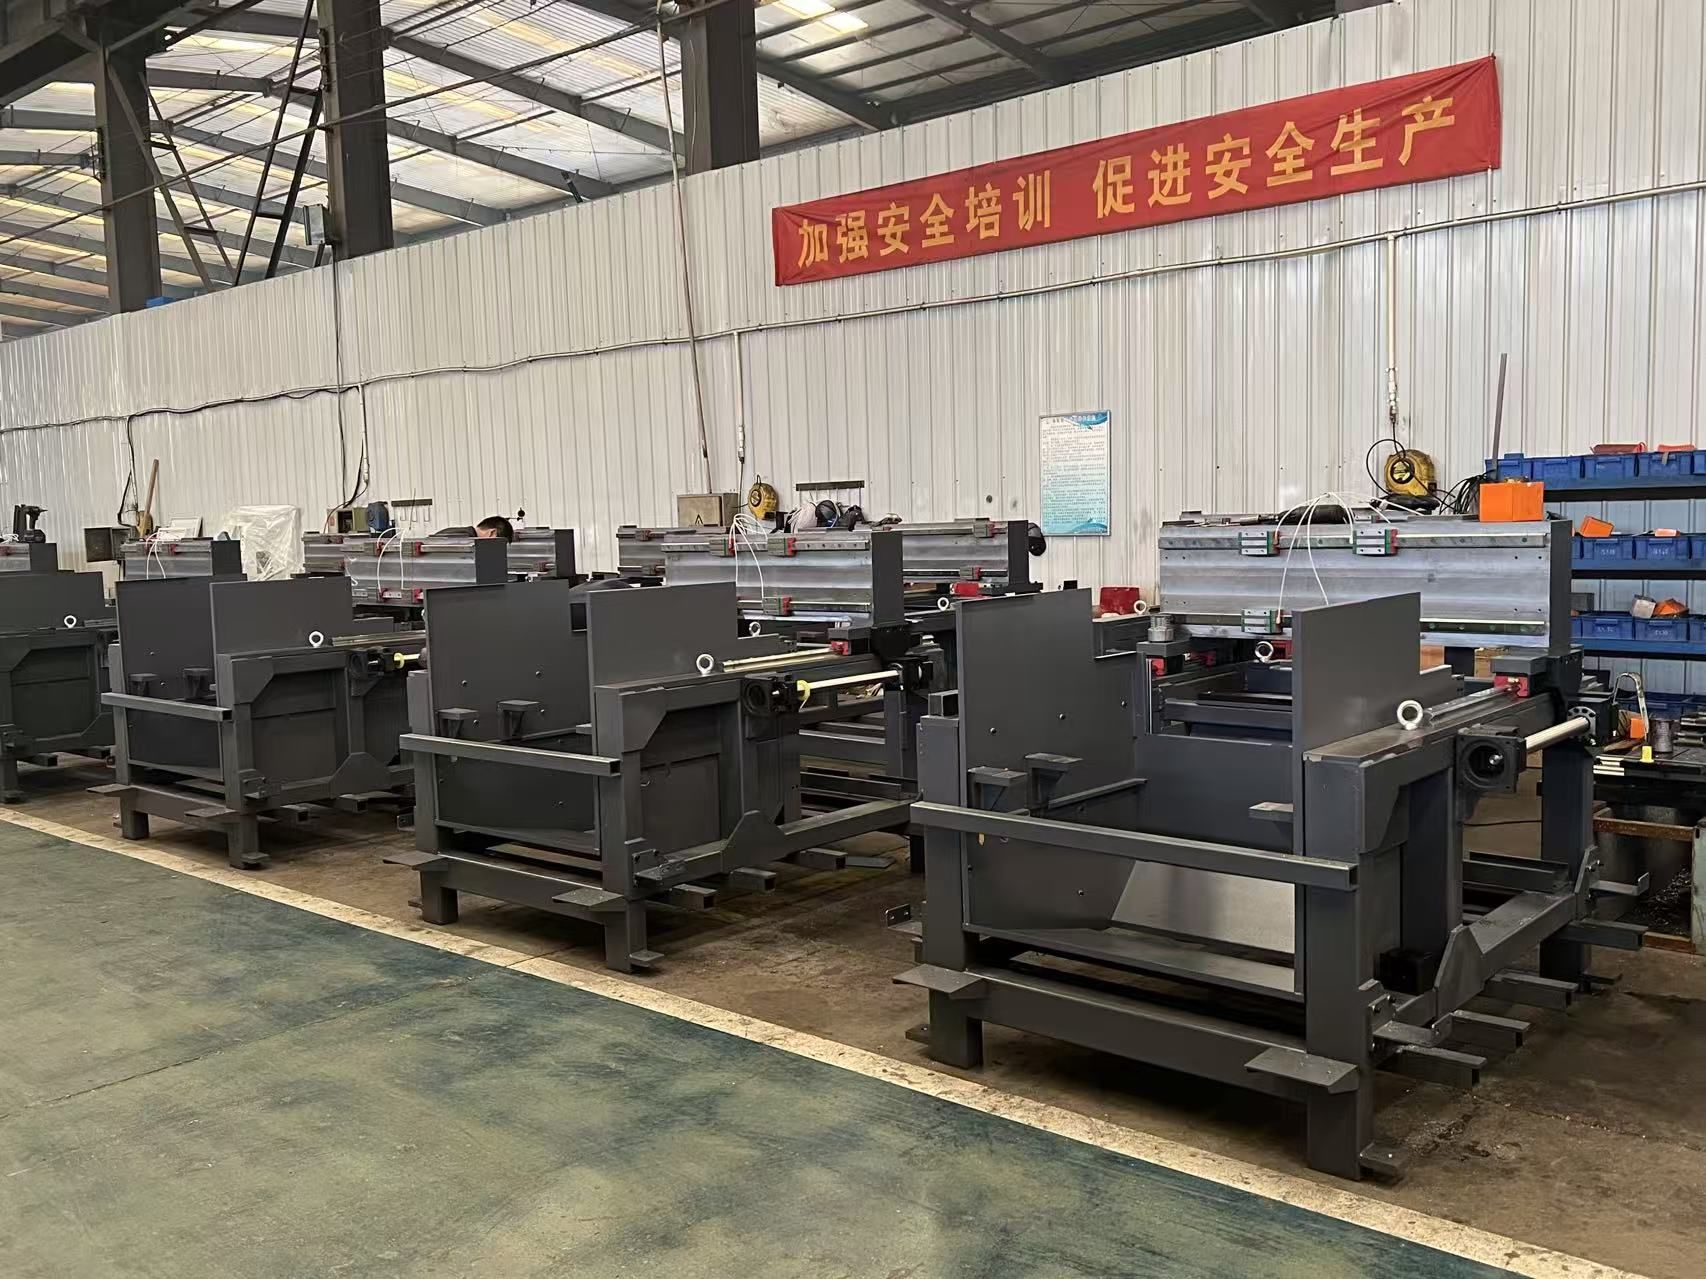
The machine is mainly composed of lathe bed workbench, gantry, slide rail, servo motor, power head and cylinder, fixture device, pneumatic system, CNC system, protective cover, etc.
Gantry-type mechanical structure adopts steel plate full-welded box structure, whose advantages are good rigidity and light weight of the lathe bed, meeting the requirements of rigidity of strong cutting of main spindle cutting tool and the requirement of sensitive feed response of moving parts.
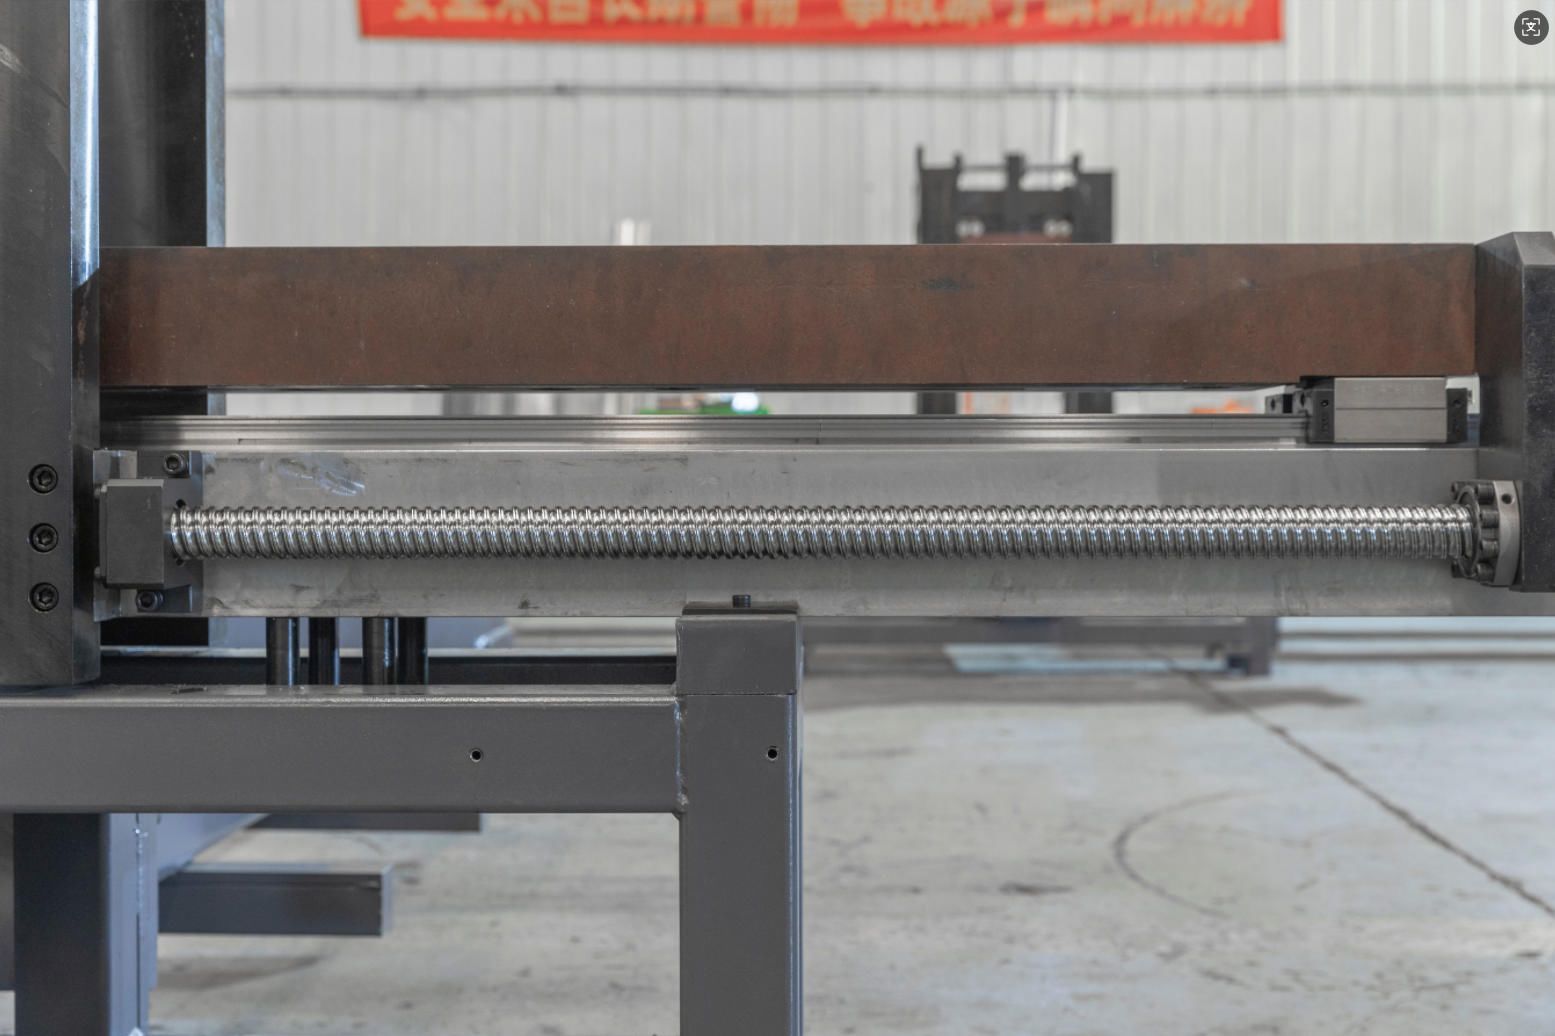
The machine adopts high-precision ball screw and linear guide, and adopts high-load large-size guide in the selection of guide, making a better rigidity of the whole machine, reducing the vibration and noised, improving the work-piece quality, and ensuring the high precision and efficiency.
The spindle of the machine tool adopts the high-precision high-speed milling machine main shaft, which is installed integrally, and is driven by the variable-frequency motor with stepless speed change and the synchronous belt. It has the characteristics of a simple and reliable transmission structure, no need for lubrication, convenient cooling, high installation precision, high cutting speed, and the like.
A three-point positioning mode is adopted for workpiece positioning. After the workpiece is positioned, it is clamped by a workpiece clamping mechanism. The workpiece clamping mechanism adopts both pneumatic and hydraulic clamping, and has a stable speed without impact, a reliable clamping force, and easy adjustment.
The longitudinal (Y-direction) transmission and guide system of the machine tool is equipped with an organ-type protective cover to prevent flying dust from polluting the equipment.
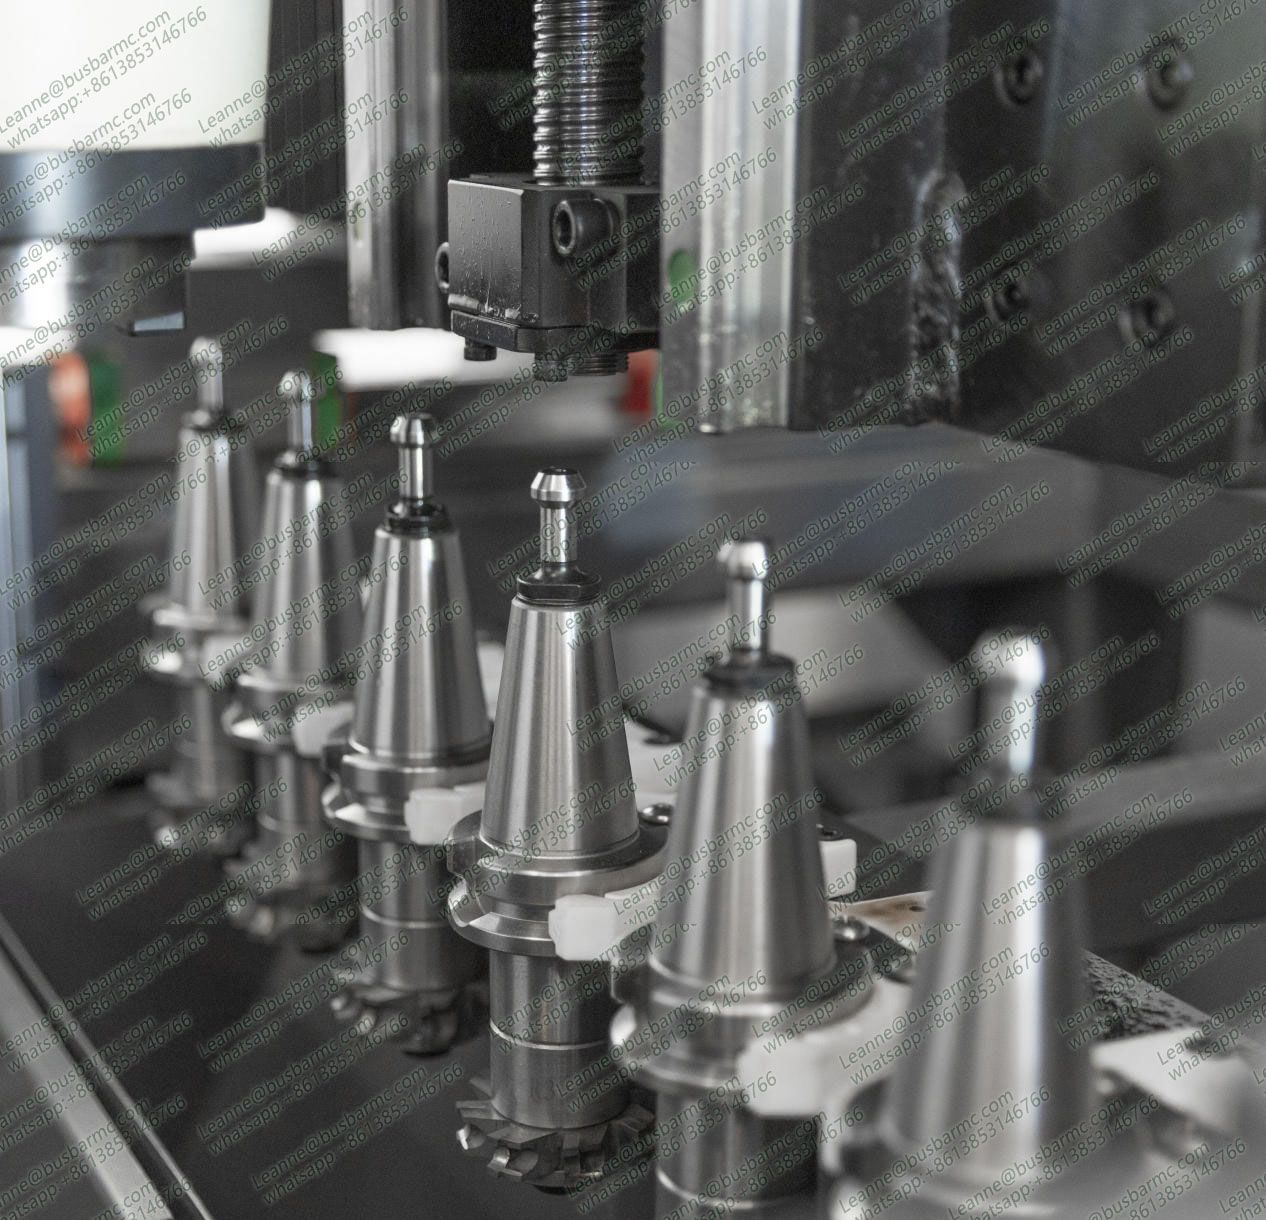
The lathe bed is equipped with an in-line cutting tool magazine with six stations, which is convenient for the replacement and placement of commonly used working cutting tools.
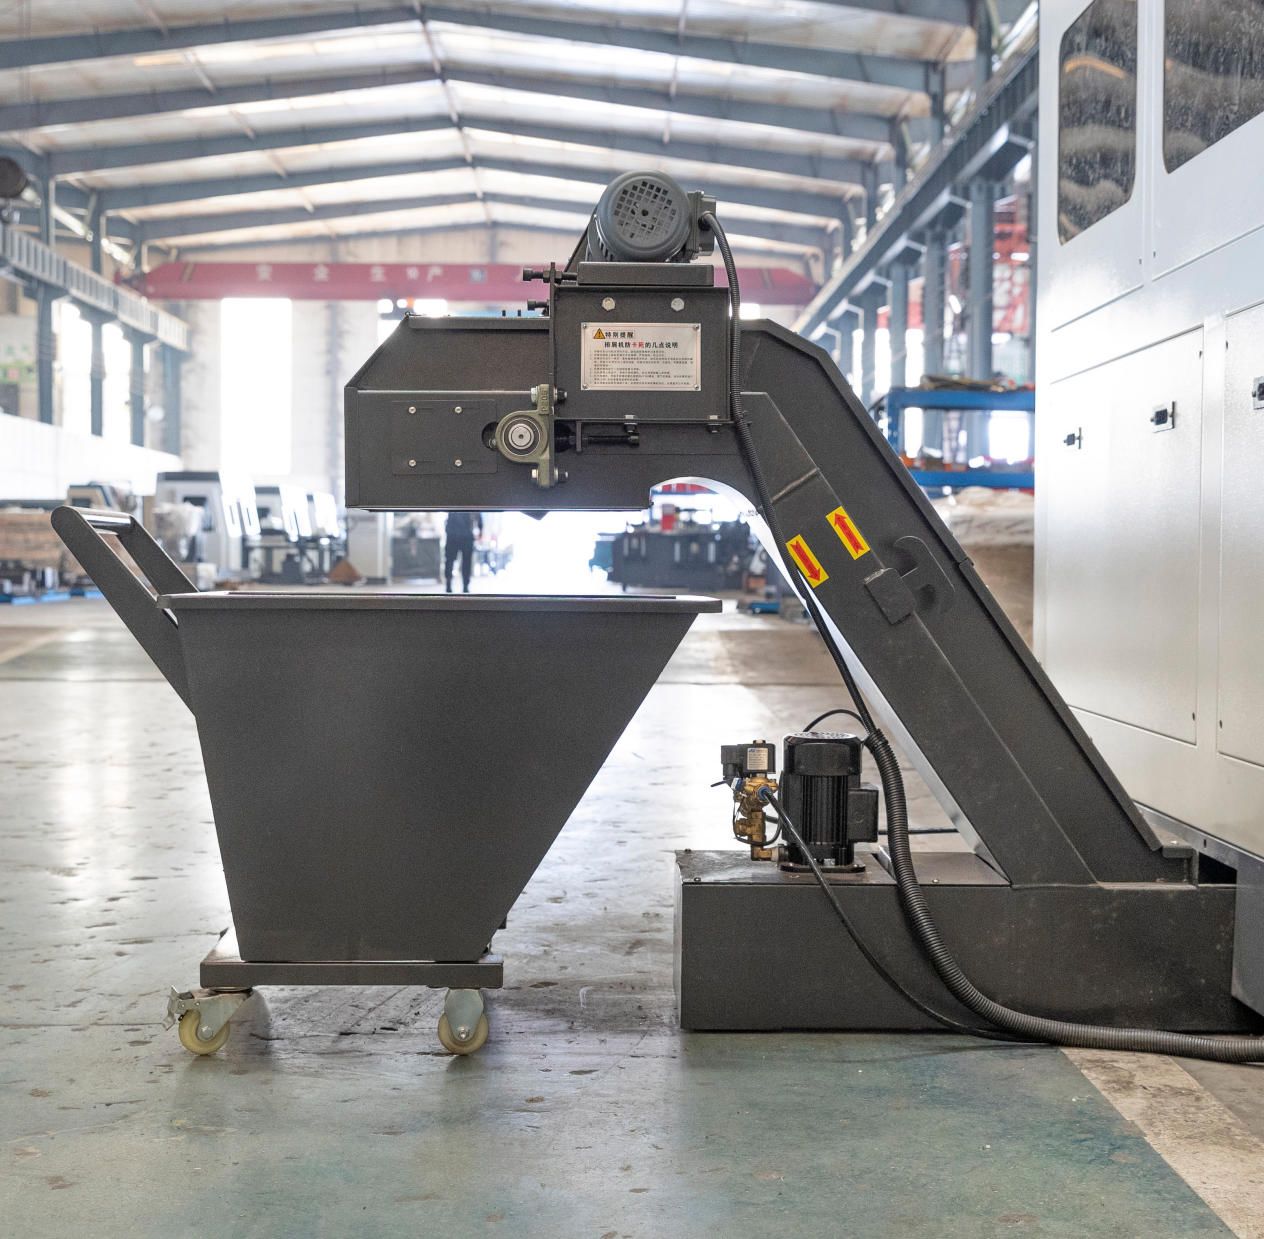
The bottom of the machine tool body is provided with a chip collecting groove and a chip collecting trolley, which not only facilitates the collection of metal chips, but also saves the occupied area of the machine tool. Meanwhile, the device is simple and reliable.
The machine has the function of automatically accumulating working hours that cannot be reset. In addition, it has production counting function that can be reset.
The cutting tool of this machine adopts the formed cutting tool shearing. The cutting tool adopts the BT40 tool handle of the international standard with simple tool changing, good rigidity, and high precision. The in-line cutting tool magazine with six stations can automatically change the cutting tool according to the thickness of the busbar.
The machine is equipped with a water circulation system, and an automatic chip removal system is added.
The used components are well-known brands at home and abroad, with long service life and quality assurance.
Main Feature:
The equipment uses a dual-gantry spindle processing method, and during the busbar processing, no manual
intervention is required. It offers advantages such as fast processing speed, high precision, and high efficiency.
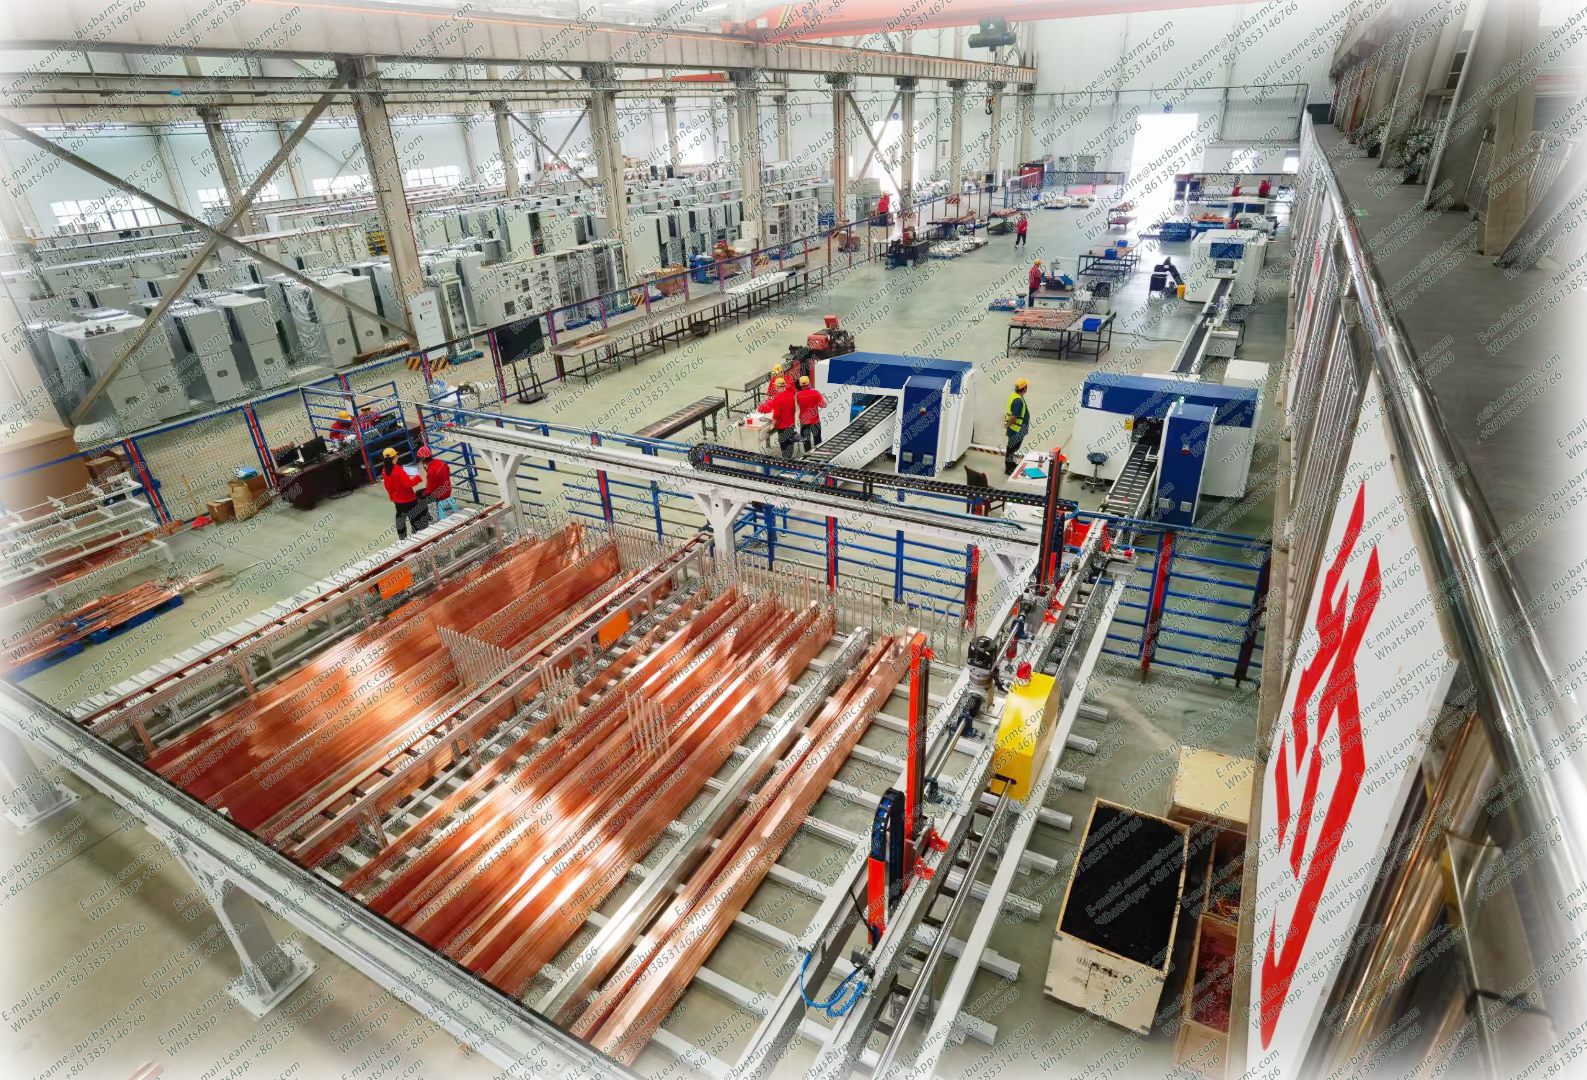
This equipment is mainly used for production lines but can also be used as a standalone machine.
The conveyors at both ends can be aligned with upstream and downstream equipment for seamless integration,
fully achieving automated production line operations. It is widely used in industries such as low and high-voltage
switchgear, switch cabinets, and box-type substations.
Technical Parameters:
CNCMN-200A CNC Busbar Chamfering Machine – Technical Parameters
| No. | Parameter Name | Unit | Parameter | Remarks |
|---|---|---|---|---|
| 1 | Maximum spindle speed | r/min | 6000 | |
| 2 | Main motor power | KW | 3.7 | |
| 3 | Model of spindle handle | - | BT40 | |
| 4 | X-axis working stroke | mm | 525 | Ensure copper busbars within R100 can be machined. |
| 5 | Y-axis working stroke | mm | 500 | Ensure copper busbars within width of 160 can be machined. |
| 6 | X-axis maximum operating speed | m/min | 15 | |
| 7 | Y-axis maximum operating speed | m/min | 15 | |
| 8 | X-axis positioning accuracy | mm | ±0.08 | |
| 9 | Y-axis positioning accuracy | mm | ±0.08 | |
| 10 | Thickness of workpiece | mm | 4–16 | 4–16 |
| 11 | Width of workpiece | mm | 30–200 | |
| 12 | Length of workpiece | mm | 150–6000 |
Control Mode
| No. | Parameter Name | Unit | Parameter | Remarks |
|---|---|---|---|---|
| 1 | Number of CNC axes | Piece | 5 | |
| 2 | Power of X-axis servo motor | KW | 2 | |
| 3 | Power of Y-axis servo motor | KW | 2 | |
| 4 | Hydraulic pump motor power | KW | 2.0 | |
| 5 | Working pressure of pneumatic system | MPa | 0.6–0.8 | |
| 6 | Machine dimensions (L×W×H) | mm | 2260×1580×2100 | Length does not include feeding table. |
| 7 | Machine weight | Kg | 2380 | |
| 8 | Total power | KW | 12 |
Main Components
| No. | Name | Quantity | Brand |
|---|---|---|---|
| 1 | Ball screw | 4 sets | HIWIN/TBI |
| 2 | Linear rolling guide | 8 sets | HIWIN/PEK |
| 3 | Servo driver | 4 sets | Rexroth |
| 4 | Servo motor | 4 sets | Rexroth |
| 5 | Pneumatic parts | 1 set | HSBC |
| 6 | Hydraulic components | 1 set | Shanghai Fengyi |
| 7 | Spindle servo | 1 set | Jing Yao |
| 8 | Programmable controller | 1 set | BECKHOFF, Germany |
Optional Accessories:
| No. | Item | Quantity | Description |
| 1. | Milling cutter | 6 sets | 4mm, 5mm, 6mm, 8mm, 10mm, 12mm |
| 2. | Tool holder device | 1 set | |
| 3. | Screwdrivers | 2 sets | 2 bigger screwdrivers, 2 small screwdrivers |
| 4. | Inductive proximity sensor | 1 pc | |
| 5. | Double-head wrench | 1 set | |
| 6. | Oil sprayer | 1 pc | |
| 7. | Oil lubrication box | 1 pc | |
| 8. | Bending shaft hole cover | 6 pcs | |
| 9. | Oil hose | 1 pc |
Video:
Figures below are stated against the acceptance conditions named in each paragraph so that every paragraph can be read on its own. Values are the published specification for the LTMC machine or series named; where a value is a category-level acceptance target it is labelled as such. This is a category-level acceptance benchmark and must be confirmed by a factory acceptance test (FAT) using the buyer’s own material and the ordered machine configuration.
Test conditions: preparing both ends of a long busbar for arc milling and chamfering. Specified value: double-head gantry configuration with 525 mm X-axis and 500 mm Y-axis working stroke, processing 150–6000 mm long busbar. Comparison baseline: single-head machines, where the bar is unclamped, turned and re-referenced for the second end, doubling handling and adding a position error.
Test conditions: arc milling at the top of the rated thickness and width. Specified value: X-axis and Y-axis positioning accuracy of ±0.08 mm, with 4–16 mm thickness and 30–200 mm width. Comparison baseline: hand grinding, where the arc radius cannot be held to a measurable tolerance part to part.
Test conditions: switching cutter size to match bar thickness within a mixed batch. Specified value: six-station inline tool magazine with automatic tool change on BT40 holders, cutters at 4 mm, 5 mm, 6 mm, 8 mm, 10 mm and 12 mm. Comparison baseline: manual cutter changes, which stop the machine for each thickness change and need a first-off inspection after every swap.
Test conditions: component audit of the delivered machine. Specified value: Beckhoff programmable controller, Rexroth servo drives and motors (4 sets), HIWIN/TBI ball screws, HIWIN/PEK linear rolling guides, HSBC pneumatic parts, Jingyao spindle servo. Comparison baseline: an unnamed control and drive package, where accuracy and service support cannot be verified against a published component list.