English
 Arabic

A CNC busbar machine improves efficiency in four measurable places: program recall instead of re-teaching, springback stored per material, fewer die changes through a turret, and a first article closer to the drawing on the first attempt, and it does not make the machine cut faster in metres per minute. Most of the gain comes from removing the adjustment loop that a manual machine needs on every new batch, because on a manual machine a large share of the day is setting up, trial bending, measuring, correcting and re-measuring rather than cutting, punching or bending. Measure setup minutes per batch and trial parts per batch before and after, in your own shop, since no vendor can predict the saving without knowing how many part numbers you repeat. A controller reduces the adjustment loop but does not remove the need for a first article check, and it will not fix a machine that is mechanically loose.
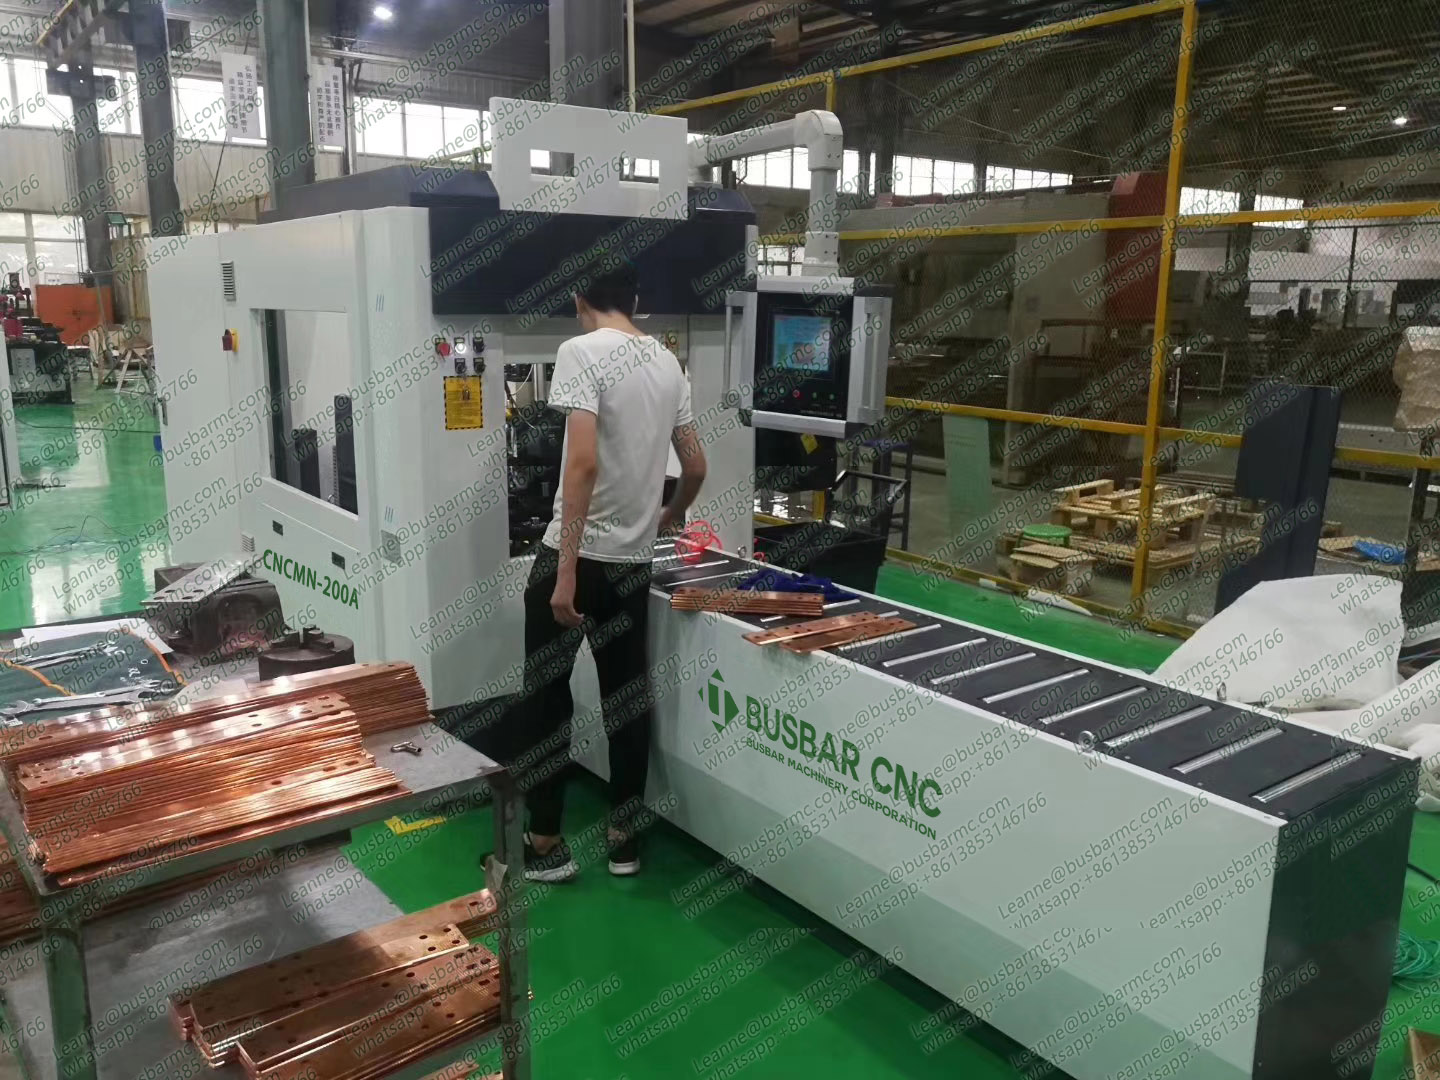
On a manual machine, a large share of the day is not cutting, punching or bending. It is setting up, trial bending, measuring, correcting and then re-measuring. When a part returns after two months, the operator who set it up last time may not be on shift, and the settings exist only in that person's memory. The next batch starts from an estimate and converges on the drawing over several trial parts. Those trial parts are scrap or rework.
This problem is sharper in GCC workshops than in European ones, because the workforce is often multinational and shift rotation is frequent. A setup that lives only in one operator's head leaves with that operator's annual leave.
A controller converts that tacit knowledge into a stored record. The bend program, the compensation value and the die used are saved against a part number. When the part returns, the operator recalls it and the first piece is close to correct. The saving is not in cycle time per stroke, it is in the number of strokes that are not scrapped.
| Lever | What changes | How to measure | Typical effect |
|---|---|---|---|
| Program recall | Setup from drawing instead of trial and error | Setup minutes per batch | Largest single gain on repeat parts |
| Stored springback | Angle correct on first piece | Trial parts per batch | Fewer scrapped first articles |
| Turret die positions | Fewer physical die changes | Die change minutes per shift | More productive hours |
| Digital bend data | Bend list imported, not typed | Entry errors per program | Fewer wrong-angle parts |
Measure these four before and after, in your own shop. A vendor cannot tell you the setup time you will save, because it depends on how many part numbers you repeat and how often they return. A shop that makes the same twenty part numbers every week will gain far more than a shop that makes a new part every day.
CNC does not fix a machine that is mechanically loose. If the die has shifted or the blade clearance is wrong, storing the program just stores the error. It does not fix material variation either: if a supplier changes the temper, the stored springback value is wrong and the first piece will be out until someone measures it. A controller reduces the adjustment loop, it does not remove the need for a first article check.
This distinction matters when a workshop is deciding between buying a CNC machine and overhauling an older manual one. If the frame is worn, the first riyal spent on a controller is wasted; the mechanical baseline has to be sound before programming adds anything.
Not materially. Hydraulic speed is set by pump and valve sizing. CNC reduces the time around the cut, not the cut itself.
Less so. If part numbers rarely repeat, there is little to recall. The value in that case is in angle accuracy on the first piece, which still helps, but the payback is slower.
Setup minutes per batch and trial parts per batch. Both are easy to record and both respond quickly to program reuse.