English
 Arabic



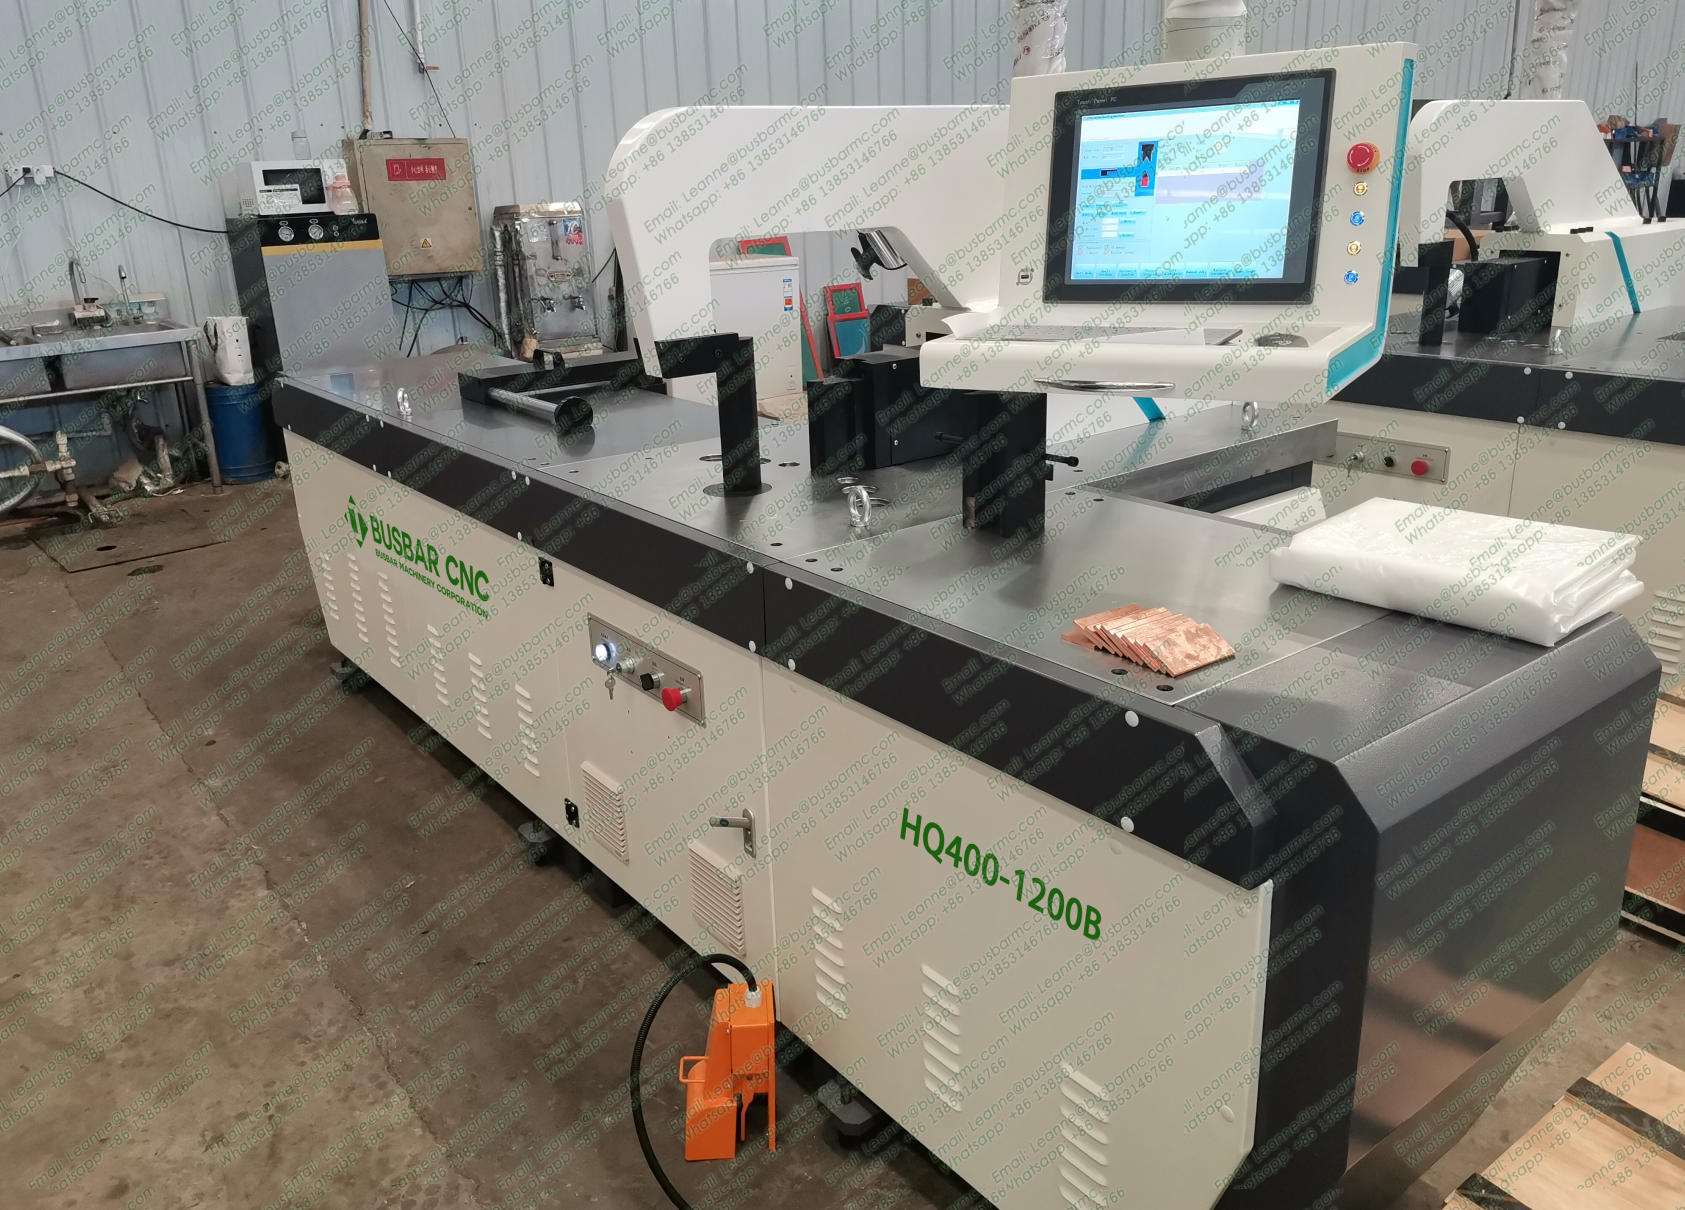
HQ.JCX-130 CNC Busduct joint connection busbar of BBT trunking system machinePro
The HQ.JCX-130 is the LTMC processing centre for BBT trunking joint connection busbar in Saudi and GCC busduct production, because it performs punching, stretching, bulging and cutting automatically on the joint busbar rather than on a plain bar. The published values are 200 kN nominal pressure, a 5 × 130 mm machining range, hole-distance accuracy tighter than ±0.1 mm, 60 strikes per minute and a 30 mm striking cylinder stroke, with X-axis positioning at up to 50 m/min on a 3600 × 1000 × 1500 mm machine weighing 1300 kg. A bar is clamped once and the automatic repeat clamp switching then indexes through the sequence with no manual intervention, which reduces scrap and raises the finished-part rate. It suits busway and busduct lines, especially joint and connection busbar runs. Confirm the joint profile and tooling against your purchase specification.
HQ.JCX-130 CNC Busduct joint connection busbar of BBT trunking system machine
Product
CNC Copper Busbar Busduct joint connection Machine
Serial
MX.JCX-130
Main Function:
Busduct joint connection busbar of BBT trunking system
Main Feature:
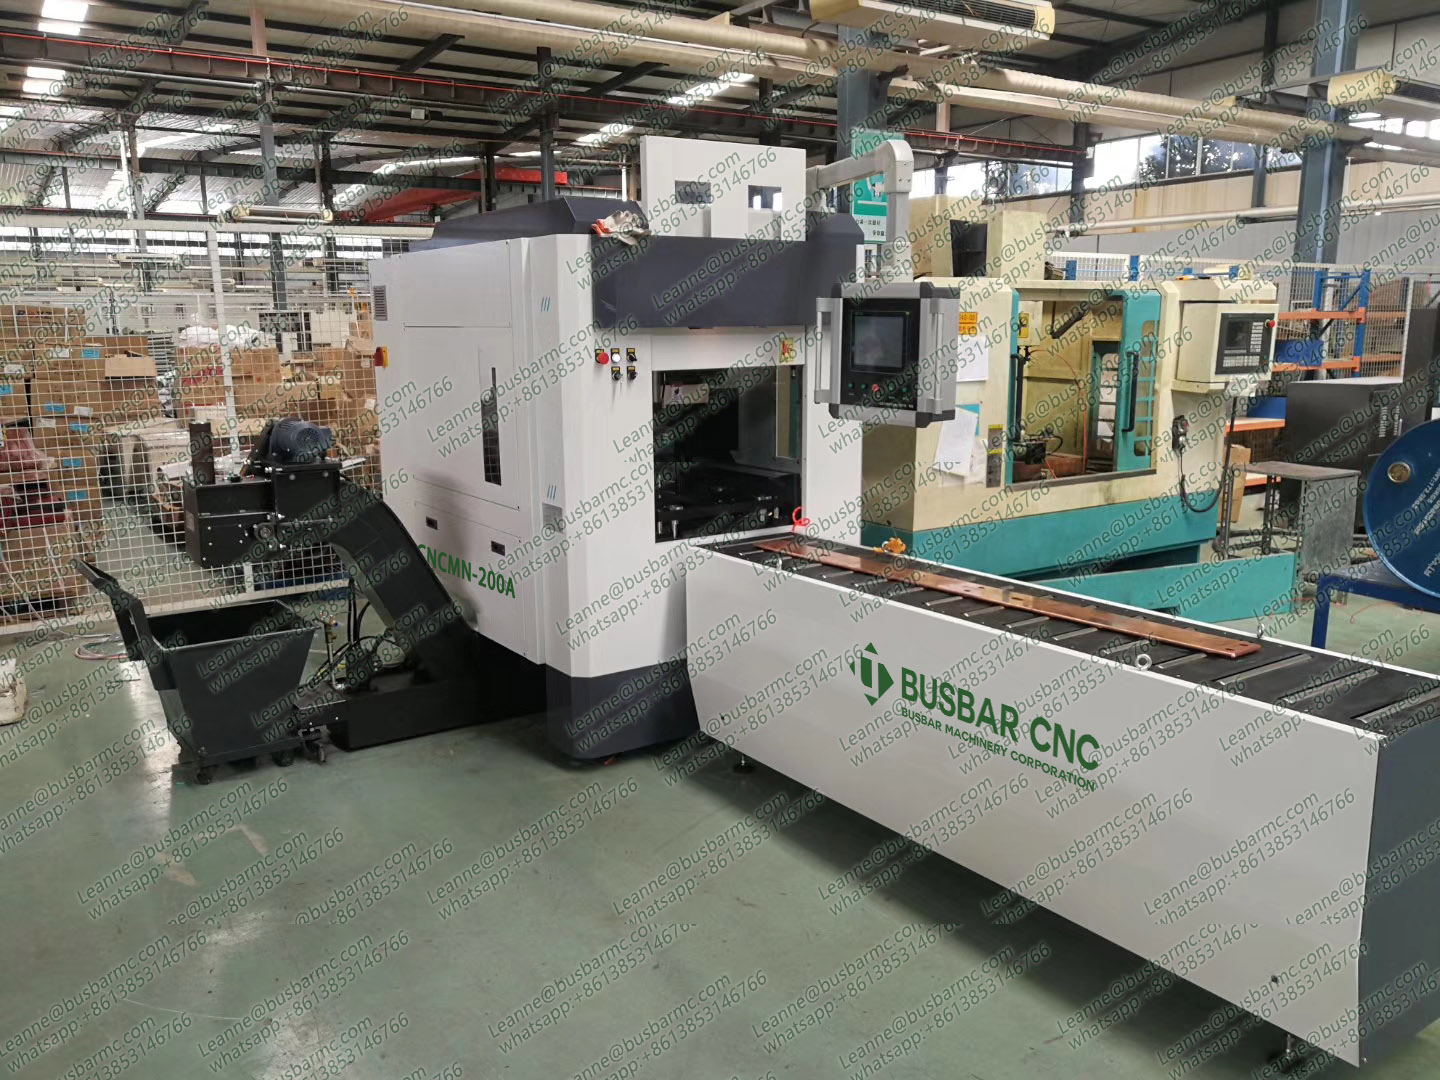
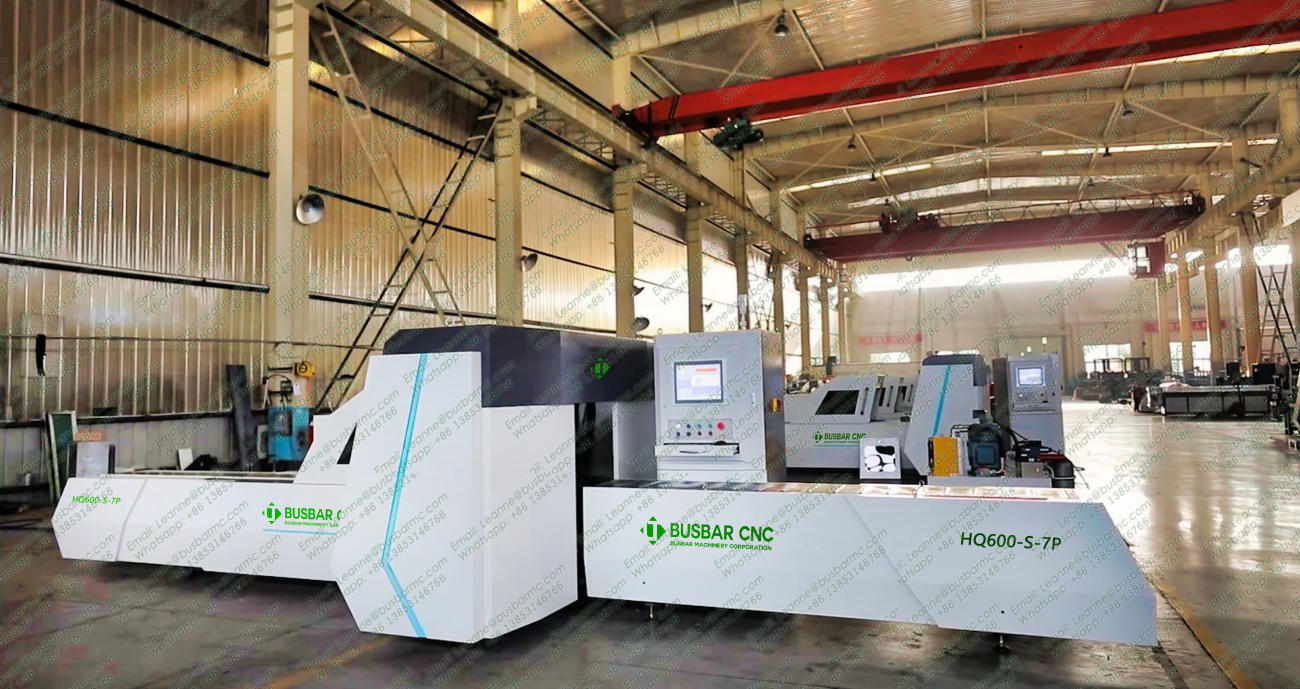
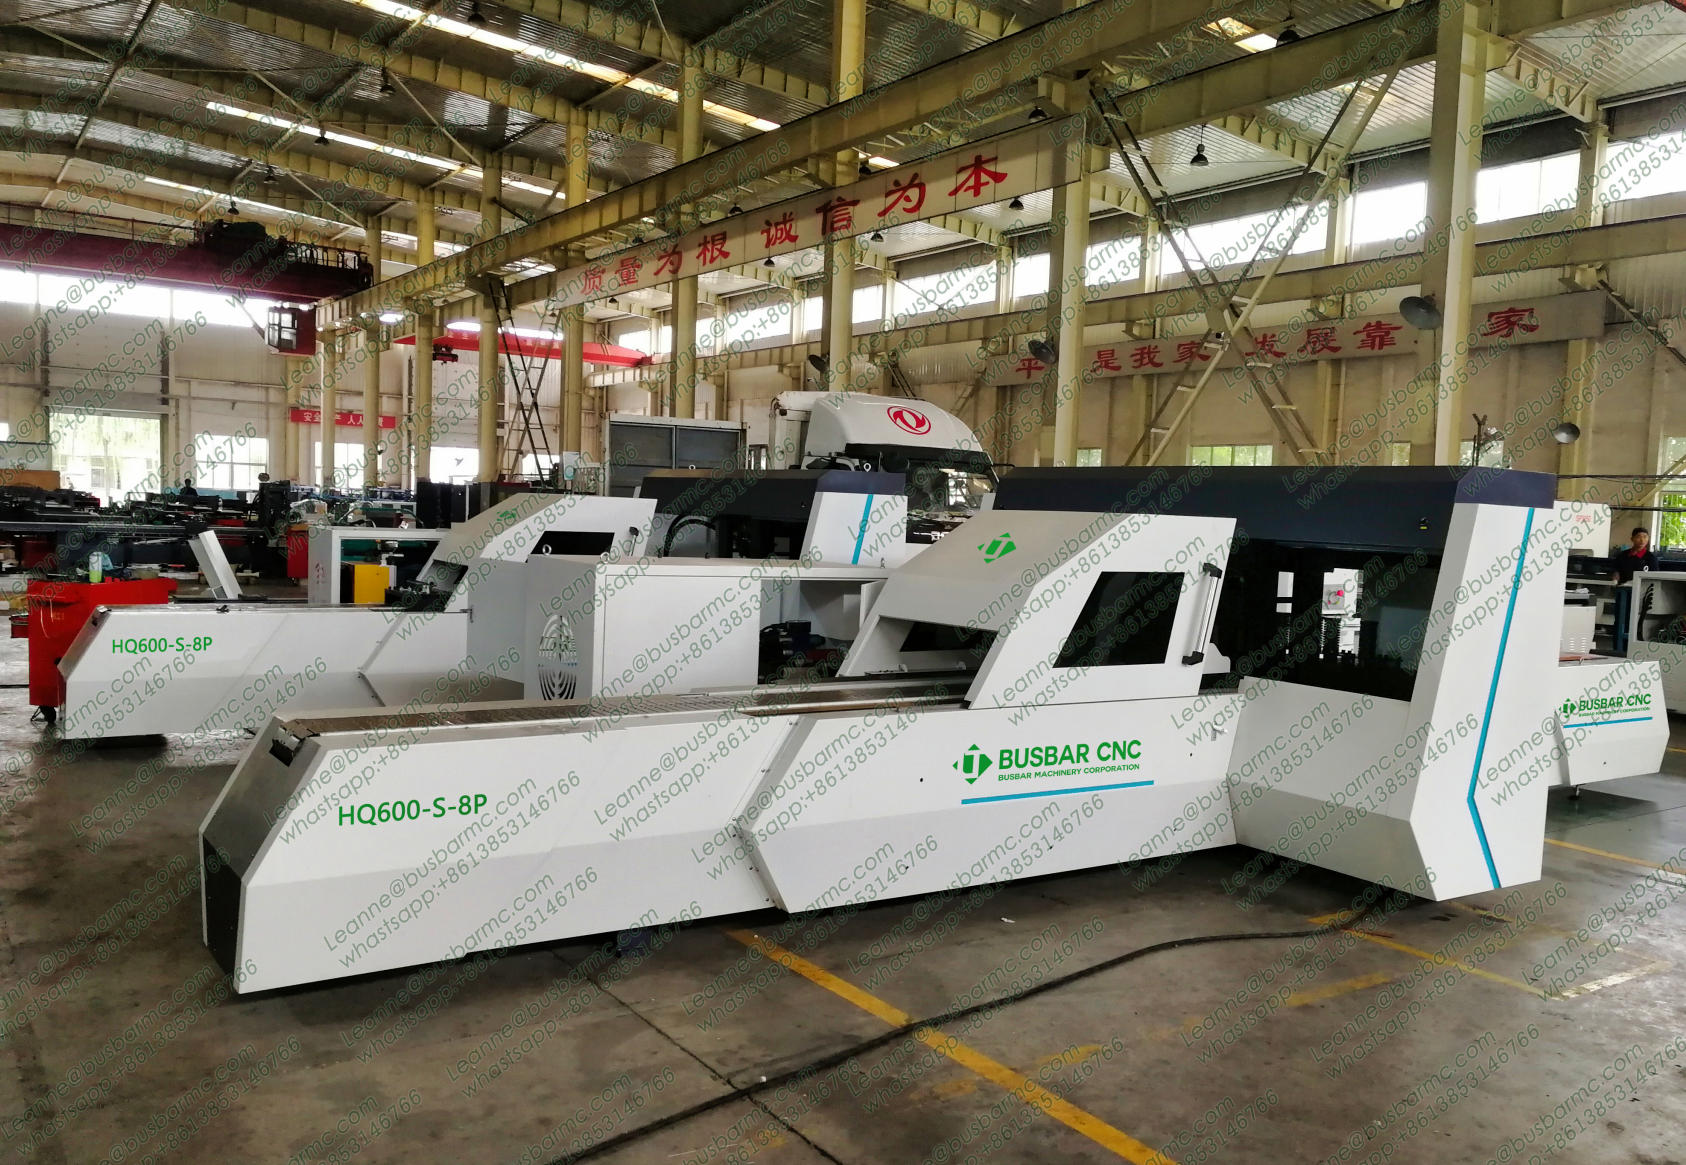
MX.JCX-130 CNC Copper Busbar bus duct disconnect switch machine CNC Bus dust connection joint bus bar processing center belongs to a new generation of processing equipment of our company that is independent researched and developed by ourselves. The main use is processing production of bus dust connection bus bar , including punching, stretching, bulging, cutting and other processing technology.
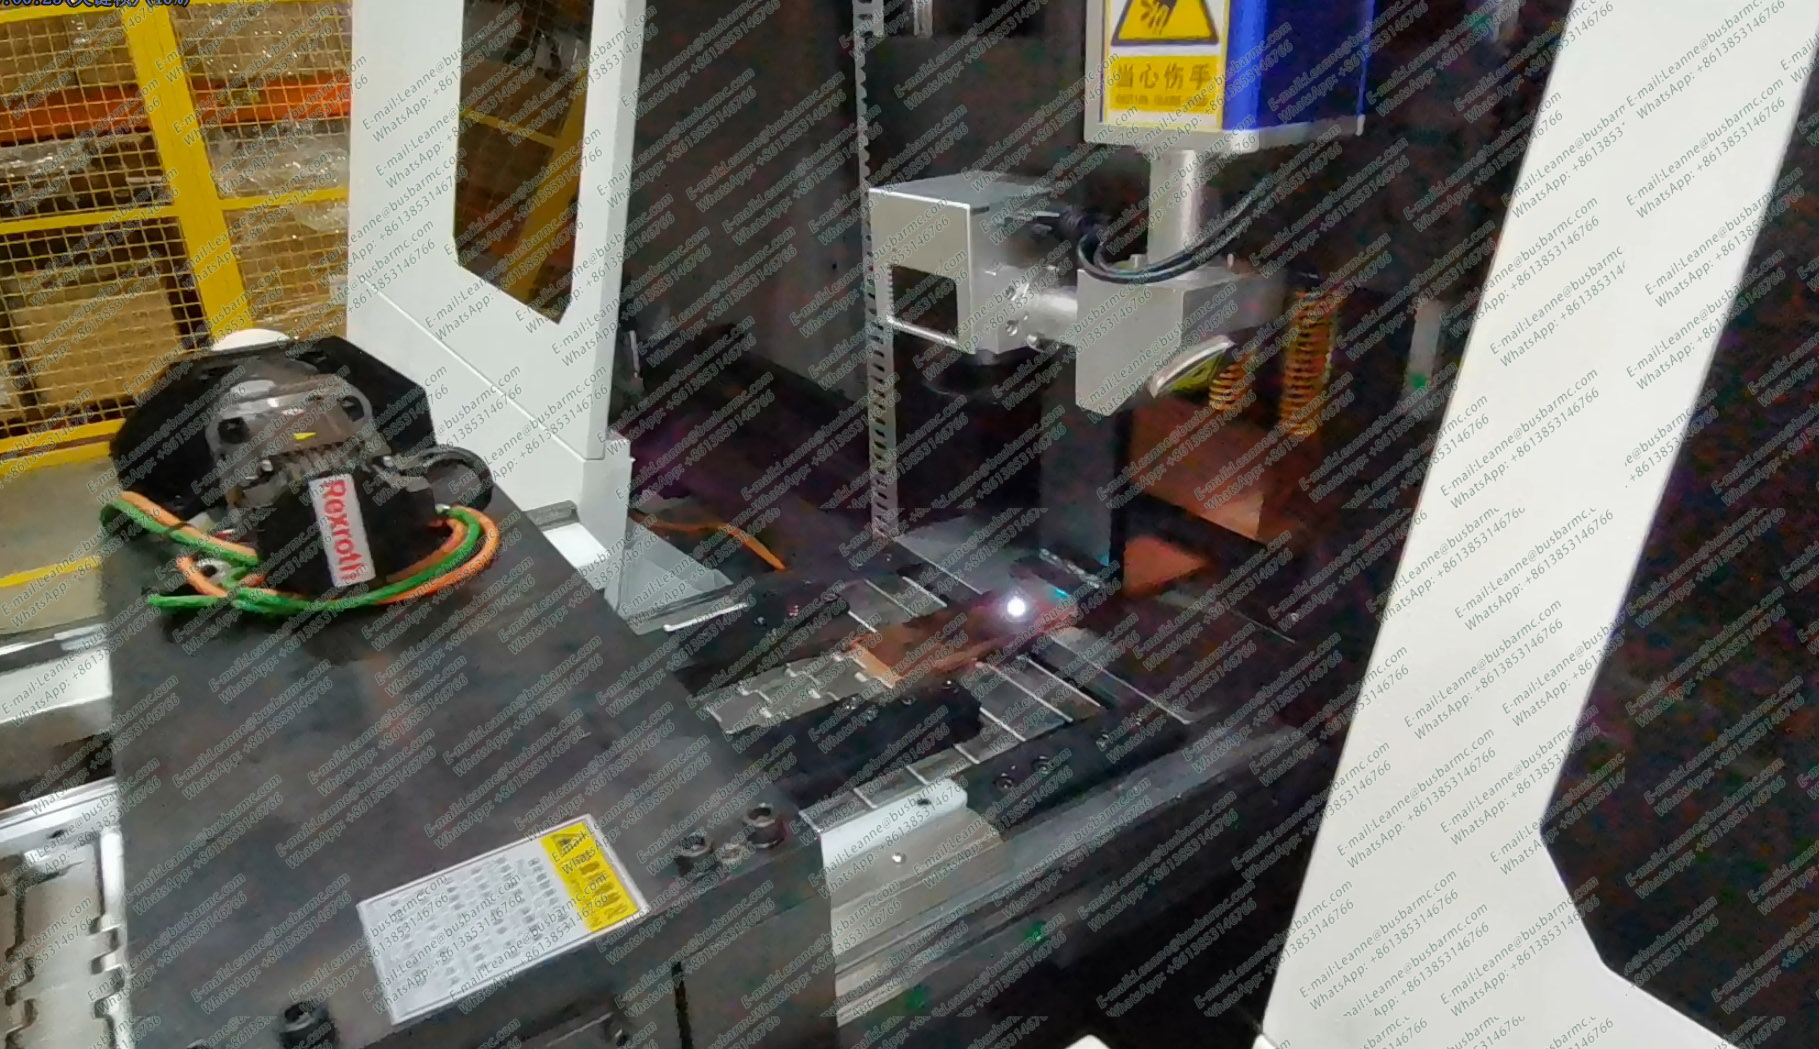
1.The main use is processing production of bus dust connection bus bar , including punching, stretching, bulging, cutting and other processing technology automatically.
2.raw materials can be realized that clamped once, without manual intervention in the process,automatic repeat switching clamp, remaining less waste, higher rate of finished products and high degree of automation.
3.The main striking head of this machine is using hydraulic work way, with the advantages of pressure strong, performance stable, the security high etc.
4.Bus bar adopts hydraulic clamp to clamp, force strong, stability high.
5.The Busway Switches machine machine adopts the man-machine interface (touch screen) dialogue, when working , simply set the relevant parameters, can be convenient to connect various technological busbar processing, has the advantages of simple operation, low requirement for the operator etc.
6.this machine adopts the transmission mode of high precision ball screw , high precision linear guide rail with the advantages of high efficiency, low energy consumption, high stability and so on.
Tech Paramete:
Nominal Pressure - 200KN
The max position speed of X axis: 50m/min
The trip for striking cylinder: 30mm
Frequency of striking: 60 Times/min
Accuracy of the distances of the holes: <±0.1mm
Machining Range: 5×130 mm
Overall size: 3600×1000×1500 mm
Weight: 1300kg
Video:
Figures below are stated against the acceptance conditions named in each paragraph so that every paragraph can be read on its own. Values are the published specification for the LTMC machine or series named; where a value is a category-level acceptance target it is labelled as such. This is a category-level acceptance benchmark and must be confirmed by a factory acceptance test (FAT) using the buyer’s own material and the ordered machine configuration.
Test conditions: punching joint connection busbar on 5 × 130 mm material with automatic indexing. Specified value: hole distance accuracy better than ±0.1 mm at 200 kN nominal pressure. Comparison baseline: manual layout and marking before punching, where ±1.0 mm hole-to-hole deviation is typical — the HQ.JCX-130 specification is about 90% tighter.
Test conditions: running the full joint busbar sequence on one clamped bar. Specified value: punching, stretching, bulging and cutting performed automatically with automatic repeat clamp switching and no manual intervention during the process. Comparison baseline: four separate operations on separate machines, each needing the part to be measured, moved and re-clamped.
Test conditions: holding the joint busbar through the full process sequence. Specified value: hydraulic clamping specified for strong force and high stability, on a high-precision ball screw and linear guide drive. Comparison baseline: mechanical toggle clamps, which relax over a long production run and let the part shift between operations.