English
 Arabic

A busbar cutting machine is judged by two measurements only: squareness of the cut face and the size of the tear zone on the offcut, and everything else including force and price is secondary to those two results. In a Saudi or GCC panel shop, blade clearance is the single most important setting on a shear, because clearance that is correct for 10 mm copper will produce a visibly worse face on 6 mm aluminum even though nothing has failed. A well-set hydraulic shear holds length to plus or minus 0.5 mm and keeps the tear zone under roughly 25 percent of thickness, which removes the deburring and secondary operations that make abrasive saws a bottleneck. When specifying a machine, always ask for the cutting capacity at the width you actually buy, because a shear rated 12 mm at 150 mm will not cut 12 mm at 250 mm.
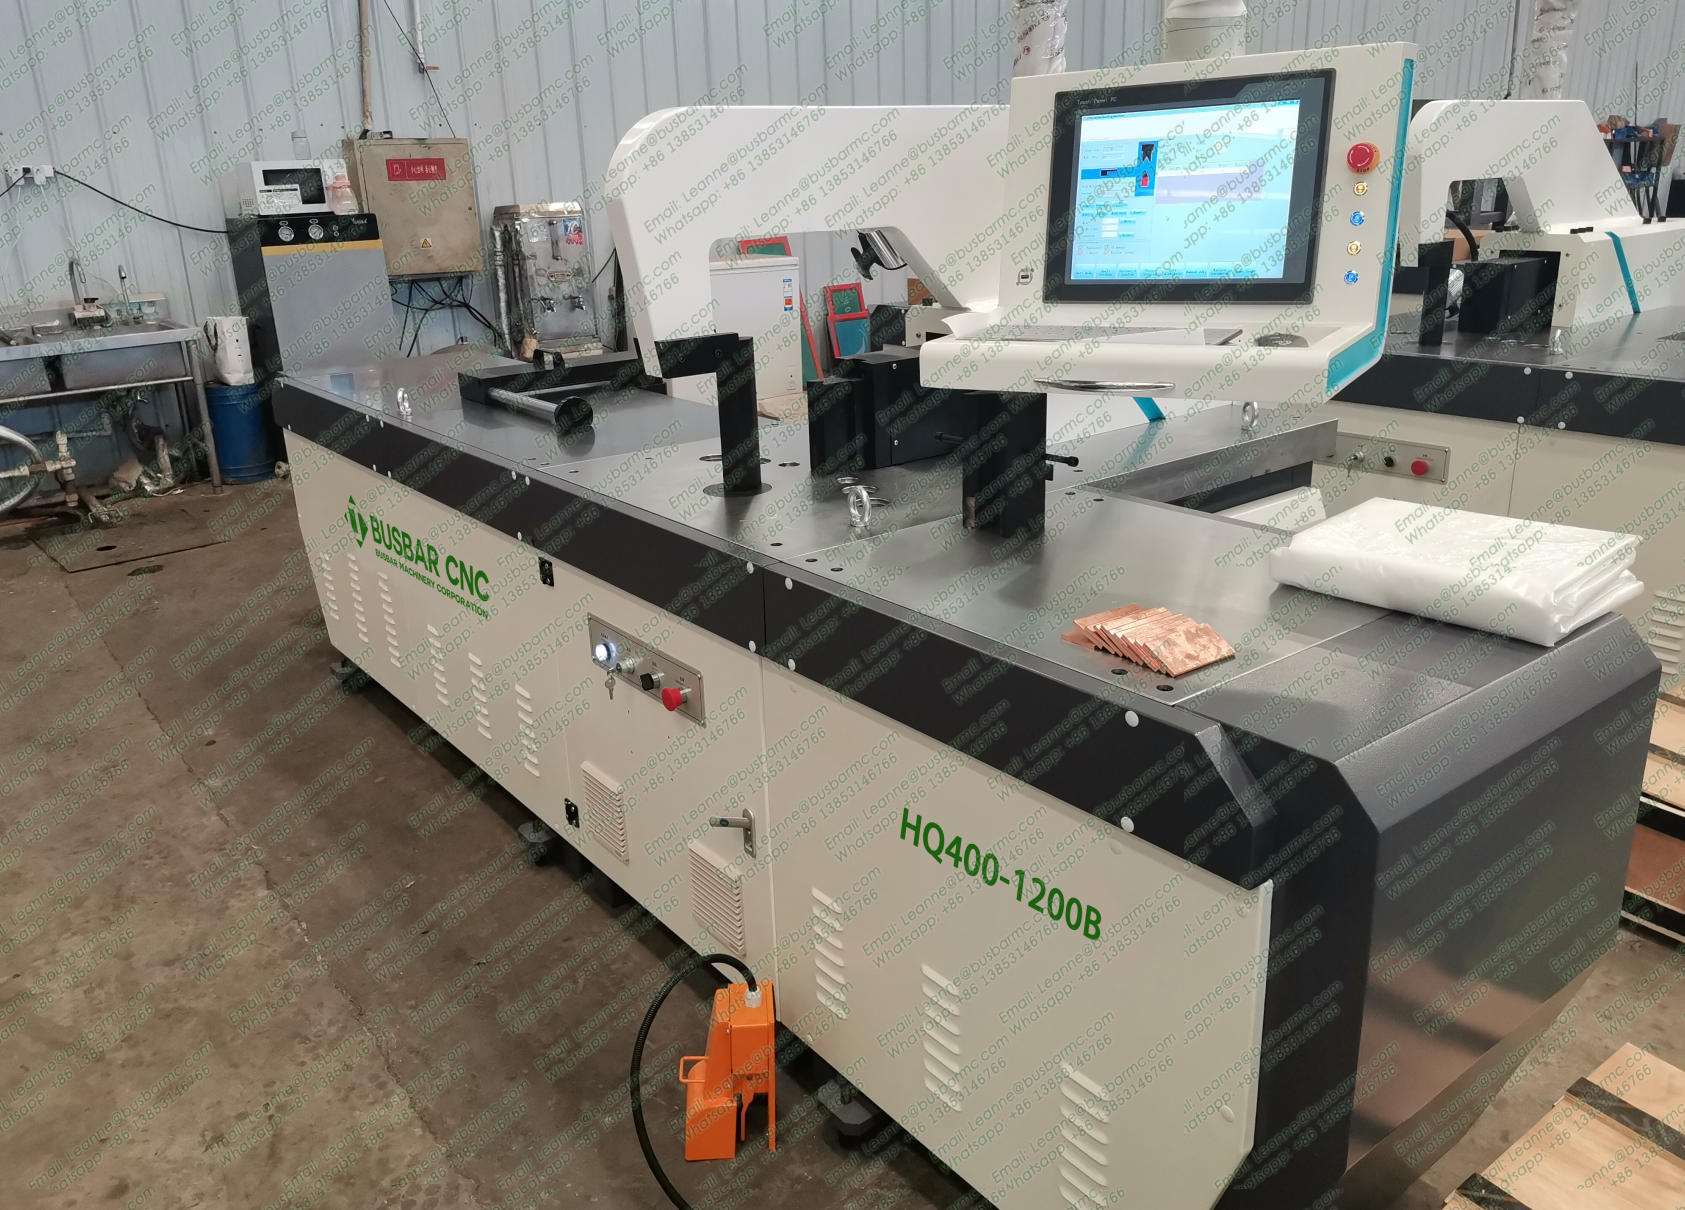
A busbar cutting machine shears flat copper or aluminum bar to finished length between two blades. Cut quality is what separates a machine that can be trusted with a drawing from one that needs a second operation. A shear does not cut in the way a saw does. It drives a blade into the bar until the material can no longer deform plastically, at which point a crack starts at the blade edge and propagates across the section.
If the blade clearance is correct for the thickness, the crack from the top edge meets the crack from the bottom edge and the face is smooth. If the clearance is too large, the cracks miss each other and the remaining material tears, leaving a rough band. That band is the tear zone. Clearance is therefore the single most important setting on a shear, and it has to change with thickness and with material.
A shear that is set for 10 mm copper and then run on 6 mm aluminum will produce a visibly worse face even though nothing about the machine has failed. This matters in GCC workshops where one machine may cut copper for switchgear on Monday and aluminum for a busduct contract on Wednesday, often with the same blade setting left in place.

| Method | Cut face | Speed | Typical use |
|---|---|---|---|
| Hydraulic shear | Good to excellent when clearance is right | Fast, one stroke | Production cutting of busbar before punching and bending |
| Abrasive saw | Rough, burr on both edges, heat affected zone | Slow | Site work, mixed material, no shear available |
| Band saw | Good face but slow and needs deburring | Slow | Thick sections, small quantities |
| CNC punch and shear line | Good, repeatable, programmable length | Fastest at volume | High volume panel production |
The abrasives and saws are legitimate ways to cut a bar, but they cost a deburring step and they cannot keep pace with a punch and bend station. In a workshop that already has a three station machine, an off-machine cut becomes the bottleneck within a week.
Published cutting capacity is usually given as maximum thickness at maximum width, and the two are linked. A machine rated 12 mm at 150 mm will not cut 12 mm at 250 mm. Ask for the capacity at the width you actually buy, not the headline number. Ask also about blade material and whether blades are reversible, because blade cost over five years can exceed the price difference between two machines.
The hold-down matters as much as the blade. If the clamp cannot hold the bar flat while the blade enters, the bar lifts, the clearance changes mid-cut and the face tears. Check that the hold-down force is independent of the cutting force, and that the clamp pad is wide enough for the widest bar you will run.
For export orders to Saudi Arabia and the GCC, two further points are worth confirming at quotation stage: the electrical build (380 V 50 Hz as standard, with 400 V 60 Hz, 415 V 50 Hz or 220 V 60 Hz available on request) and the spare blade and seal package, because air freight for a single blade costs more than the blade itself.
Blades wear on the corner first, and a worn corner shows up as a burr on one end of the bar only. Rotating or reversing blades on a schedule keeps the face consistent for longer than waiting for a visible failure. Check blade clearance after any change of material thickness, and clean the blade seat, because a chip under the blade tilts it and produces a taper across the width.
In most panel shops, yes. The cutting station on a three station machine uses the same shear principle and the same clearance logic. A dedicated shear wins on cycle time and on very thick sections, not on face quality.
That is the tear zone, and it usually means the blade clearance is too large for the thickness, or the blades are worn, or the hold-down is not holding the bar flat.
A light deburr is normal practice on copper because the cut edge work hardens. If the shear is set correctly the burr is small and a hand tool is enough. A heavy burr means the process is out of adjustment, not that you need a bigger deburring machine.